Find ATEX, IECEx, Explosion Protection & Hazardous Area Content...

News

University of Huddersfield academic and advanced nuclear materials expert is named winner of three global awards

joe.jpeg

University of Huddersfield academic and leading expert in advanced nuclear materials, Professor Konstantina Lambrinou, has been named the winner of three global awards by The European journal.

Professor Lambrinou has been honoured in The European Awards 2025 three times over, as the recipient of the following awards:

 - Excellence in Nuclear Engineering Award 2025

 - Clean Energy Materials Visionary Award 2025

 - Woman of The Year for STEM Leadership Award 2025

Professor Lambrinou is Professor of Advanced Materials at the School of Computing and Engineering at the University of Huddersfield. Her research interests revolve around the accelerated development of advanced nuclear materials, including accident-tolerant fuels (ATFs).

Professor Lambrinou is the coordinator of the H2020 IL TROVATORE project, an international collaboration involving 30 partners from the EU, the USA and Japan, funded by H2020 Europe’s Euratom Research and Training Programme.

She is also the coordinator of the HORIZON SCORPION project, an international collaboration involving 16 partners from the EU, the UK, the USA, Japan, and Switzerland, funded by Horizon Europe’s Euratom Research and Training Programme. Moreover, she is the European lead of the I-NERI US/EURATOM PERSEUS project, and the technical lead of a Westinghouse-led GAIN VOUCHER program funded by US-DOE.

The above projects focus on innovative ATF cladding materials, the development of which is driven by the demand for enhanced nuclear energy safety in the aftermath of the Fukushima Daiichi event in 2011.

Of the triple honour, Professor Lambrinou commented: “I was really caught by surprise back in November 2025 when they called me from The European to inform me that I won three awards, as I was not even aware of the journal’s online voting system. For me, these awards are not only a great honour but also a recognition for 15 years of hard work in the field of nuclear materials science and engineering.”

Professor Leigh Fleming, Acting Dean - School of Computing & Engineering, commented: “I am delighted that Konstantina has been honoured with these awards; they are a testament to her hard work and dedication to research. She has developed unique expertise in the field, and I am so delighted that it has been recognised with such a prestigious accolade.”

The European offers expert coverage of finance, technology, energy, leadership and emerging market trends and holds a position as a trusted source of high-quality global business insight.

Its annual awards programme celebrates achievement, innovation and excellence, with nominations submitted through an online voting system.

The awards team detailed that Professor Lambrinou, especially in leading the HORIZON SCORPION international collaborative project, was highly deserving of these awards for its pioneering development of revolutionary ATF cladding materials.

They added that the project not only enhances the inherent safety of future nuclear energy but also demonstrates exceptional international cooperation in addressing one of the most critical challenges facing the global power industry today.

Professor Lambrinou has featured in The European on multiple occasions, including on the front cover of its Spring 2025 edition, under the heading CORE STRENGTH: Prof Konstantina Lambrinou leads Europe’s race to engineer nuclear materials tough enough for Earth – and beyond.

HSE announces changes to leadership to Energy Division

HSE.jpeg

Britain’s national regulator has announced leadership changes to its Energy Division, which regulates the offshore oil and gas industry and renewables and onshore gas networks, mines and quarries.

Samantha Peace, who has held the position of Director of Energy Division at the Health and Safety Executive (HSE), will retire in May after serving the regulator for more than 30 years.

Samantha, who has worked in the public sector for 38 years, has held the role since July 2023, overseeing the health, safety, and welfare of workers across the offshore and renewables industries, and supporting the deployment of technologies such as Carbon Capture, Utilisation and Storage (CCUS).

Matthew Blackburn has been appointed as interim Director of Energy Division and will take over from February 16 to allow for a smooth and structured handover to take place. Matthew, currently Operations Manager in Energy Division, has more than 27 years’ major hazards experience in HSE.

Jane Lassey, Director of Regulation at the Health and Safety Executive, said: “I would like to thank Sam for her dedication throughout the last 30 years at HSE and, more recently her leadership over the last three years.

“Energy Division is responsible for some of the most important, and most hazardous, industries in Britain, and Sam has played an important role in our efforts to maintain safety, while working with industry as an enabling regulator.”


Do you understand the changes to IEC 60079-14:2024?

Published in August 2024, the latest update to IEC 60079-14 introduces mandatory compliance requirements for products used in explosive atmospheres — including a major shift in how cable and cable gland selection is assessed.

To help manufacturers navigate these changes, Element has partnered with explosive-atmosphere expert Jonathan Hitchens (InsightEx) to break down what’s changed and what it means in practice.

📘 This expert whitepaper covers:
• Drivers for change in IEC 60079-14:2024
• The move from individual component assessment to system assessment
• Key technical changes affecting cable and cable gland selection
• Impact on manufacturers and wider industry
• Transitional considerations and global adoption

Understanding these updates is critical to ensuring compliance and avoiding costly errors.

👉 Download the whitepaper today

#IEC60079 #ExplosiveAtmospheres #HazardousAreas #ATEX #Compliance #FunctionalSafety #Engineering #Manufacturing #ProcessSafety

Major chemical firm hit with £400,000 fine after dangerous steam release

A global chemicals company has been fined £400,000 after a worker narrowly escaped serious injury in a high-pressure steam release incident at its site in Huddersfield.

Syngenta Ltd was sentenced after the 59-year-old contractor – working under its control and direction – had been carrying out unsafe maintenance work. The man had been working as a mechanical fitter on 6 November 2023 when the incident took place, resulting in the company reporting it to the Health and Safety Executive (HSE) as a dangerous occurrence. The incident involved a release of high-pressure steam as he went about his job.

The company operates a large agrichemicals production site where some of the production plants rely on high pressure steam to manufacture products. The HSE investigation found that the incident occurred during the planned replacement of a faulty steam trap on small-bore pipework.

Steam traps are devices that automatically remove condensate (water) and air from the high-pressure steam system. There was a sudden failure of the valve used to isolate the work location from the steam, and this resulted in the uncontrolled high-pressure release.

The HSE investigation also revealed several failures with the system of work in operation. These included:

  • The isolation valve failed when the mechanical fitter was separating a bolted flange by cutting the bolts using a battery powered reciprocating saw.
  • The isolation valve and flange bolts were affected by corrosion and were in a poor condition.
  • Due to widespread corrosion of flange bolts on the steam distribution system, it was considered necessary to routinely cut bolts rather than unscrew them using a spanner.
  • Cutting flange bolts reduces the ability to control any unexpected, trapped material or pressure remaining in the pipework.

Syngenta Ltd pleaded guilty to having failed to ensure that the isolation valve and flange bolts were maintained in an efficient state, in efficient working order and in good repair – as required by Regulation 5(1) of the Provision and Use of Work Equipment Regulations 1998 (PUWER) – HSE.

In addition, there was an issue with the company’s documented risk assessment procedure in place before such maintenance work was undertaken. It was routine for Syngenta to carry out maintenance work on small-bore pipework of the high-pressure steam distribution system, using a single method of isolation.

HSE’s published guidance about on this subject (The safe isolation of plant and equipment – HSE, HSG253) emphasizes that using a method of double isolation is safer. The risk assessment documents in place failed to appreciate the increased risk involved in relying on a single method of isolation when there was known corrosion of the work equipment. Syngenta Ltd also pleaded guilty to having failed to make a suitable and sufficient assessment of the risk involved in carrying out the specific maintenance work described as required by Regulation 3(1) of the The Management of Health and Safety at Work Regulations 1999.

Syngenta Ltd, whose head office is at Bracknell, Berkshire pleaded guilty to the two offences at Leeds Magistrates’ Court on 28 January 2026 and was fined £400,000 and ordered to pay costs of £8,288.

HSE Inspector David Welsh said: “If a safe system of work had been in place at the site when the maintenance was being carried out, this dangerous incident would not have happened.

“The company did not appreciate the extent of the risk posed because of the way the maintenance work was being done, and the relatively simple control measures that could have been applied to make it safer.

“Syngenta not only failed produce an appropriate risk assessment, but also failed  to maintain work equipment in a safe condition – which taken together meant that this was a dangerous accident waiting to happen.”

This HSE prosecution was brought by enforcement lawyer Iain Jordan and paralegal officer Zara Salman.

Further information:

  1. The Health and Safety Executive (HSE) is Britain’s national regulator for workplace health and safety. We are dedicated to protecting people and places, and helping everyone lead safer and healthier lives.
  2. More information about the legislation referred to in this case is available.
  3. Further details on the latest HSE news releases is available.
  4. Relevant guidance can be found here: The safe isolation of plant and equipment – HSE
  5. HSE does not pass sentences, set guidelines or collect any fines imposed. Relevant sentencing guidelines must be followed unless the court is satisfied that it would be contrary to the interests of justice to do so.  The sentencing guidelines for health and safety offences can be found here.

​

Gas explosion proof extruder motor in size 1000

mENZEL.jpeg

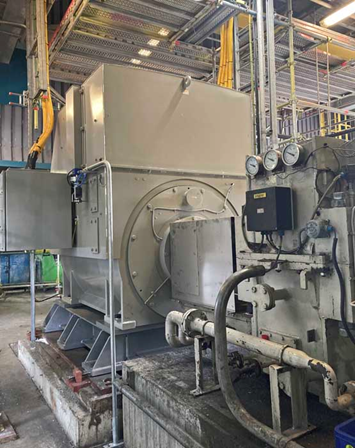
Replacing an explosion-proof size 1000 motor at short notice is an ambitious task. For the German family-run company Menzel Elektromotoren, it was a chance to prove once again its extensive expertise in the design, manufacture and certification of explosion-proof motors. A plastics producer had to replace an existing extruder motor with ignition protection type Ex d (flameproof encapsulation) very urgently. Menzel and the client found that a motor with the ignition protection type Ex ec (increased safety) would satisfy the current hazardous zone requirements. The motor manufacturer selected a suitable three-phase squirrel-cage motor from its extensive stock, individually adapting it for the drive task and the installation site. The project hinged on upgrading the motor for zone 2 hazardous areas with potentially explosive gas atmospheres and getting it the necessary ATEX certification. Menzel’s officially certified in-house experts labeled the motor II 3G Ex ec IIC T4 Gc. The new motor with a lower shaft height at 630 mm was brought up to the center height of the old motor by means of a welded base. Since the new motor has four winding systems instead of the two of the old one, Menzel also made electrical modifications for operation on the existing frequency converter.

FASTTRACK.jpeg

Fasttrack customization and certification for hazardous areas – the extruder motor is now already in use and the customer is satisfied

The project exposes the existing supply gap for explosion-proof motors in large sizes: the few existing suppliers can only offer building a motor from scratch – with the corresponding months-long delivery times. Menzel stands out from the competition with its large stock inventory and ability to configure and adapt stock electric motors in-house for hazardous areas and certify them according to the latest ATEX

directives. In this instance, only two weeks passed from order placement to installation at the customer’s site. The customer came to Berlin for testing and acceptance and praised Menzel’s flexibility.

More about motors with ignition protection type Ex ec (increased safety) for zone 2 or 22 hazardous areas with gas or dust atmospheres: https://www.menzel-motors.com/ex-na/

aemt.jpeg

Load testing of supersized vertical motors

MENZEL_jAN_26.jpeg

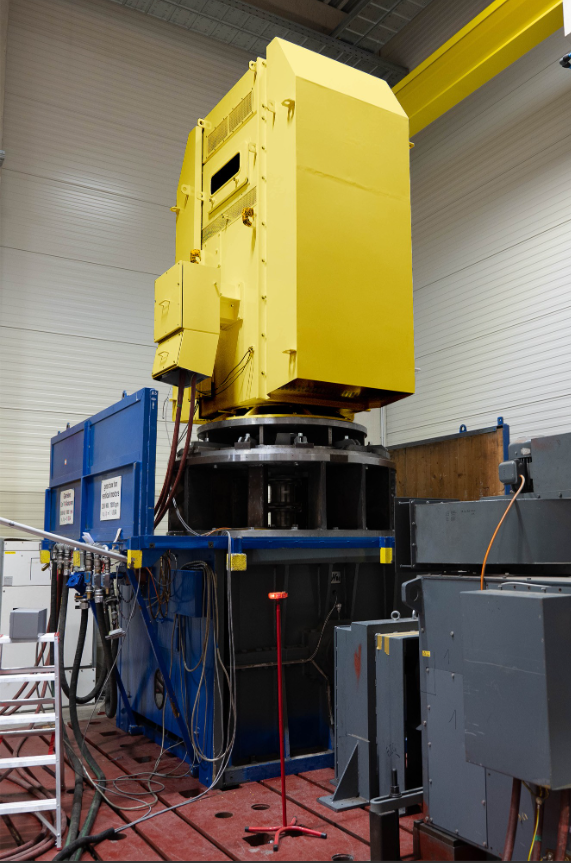
Menzel Elektromotoren now also performs load tests on motors in a vertical installation position. The family business has expanded its in-house test field to include a right-angle gearbox with various flange options for vertical motors of different sizes. This enables thorough testing of vertical motors for pumps, compressors and other industrial applications under realistic load conditions. Menzel tests motors and generators from its own production and also offers its state-of-the-art test facilities for manufacturer-independent external tests. The plant in Hennigsdorf near Berlin has two large test stands. Indoor cranes with a hook height of 7.52 meters shift large drive units up to 80 tons. The range of services includes all common routine, type and system tests in accordance with international standards for test voltages from 3 to 13.8 kV. Machines up to 1800 kW and 2300 kVA can be load tested. In addition, Menzel offers a heat run test with the equivalent load method according to IEC60034-29 for higher electrical performances. The test field engineers and certified technicians carry out all measurements and inspections according to EN 60034, with full documentation. The team also has extensive expertise in testing requirements of international acceptance organizations.

Detailed information about Menzel’s testing services and facilities: https://www.menzel-motors.com/motor-test-field/

Documentation: The Hidden Backbone of ATEX and IECEx Certification

exveritas_jan_21.jpeg

For manufacturers of equipment intended for explosive atmospheres, technical documentation is not a formality it is foundational to ATEX and IECEx certification. Certification bodies primarily assess conformity through the documented evidence provided. If that evidence is unclear, incomplete, or inconsistent, even well-designed equipment may face delays, redesign, or rejection.

iecex_a.jpeg

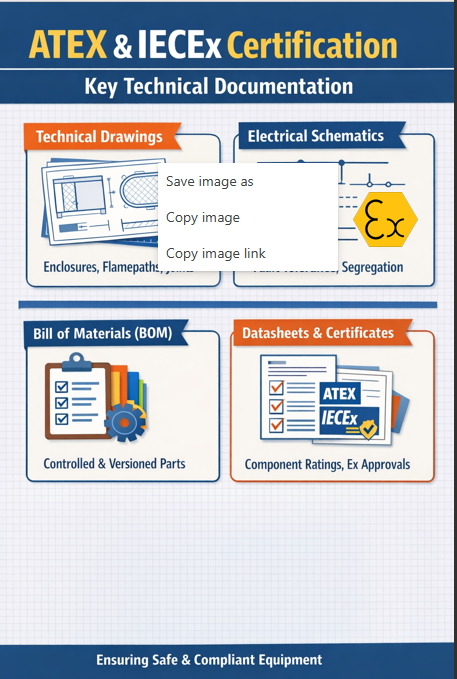
Drawings and Schematics Define Safety General arrangement and assembly drawings define how the equipment is built. These include details such as enclosure construction, joint types, fasteners, sealing methods, and clearances—all vital to verifying the chosen protection concept (e.g. Ex d, Ex e, Ex i, Ex p, or Ex t). Certification assessors use these drawings to confirm that the protection concept has been applied correctly and consistently. Gaps in documentation inevitably trigger technical queries.

Electrical schematics are equally important. They provide visibility into circuit topology, protection devices, segregation of circuits, and interfaces between hazardous and safe areas. In methods like intrinsic safety or increased safety, the schematic is central to assessing energy limitation, fault tolerance, and standard compliance. Poorly structured schematics are a common source of late-stage non-compliances.

BOMs and Datasheets Build Confidence A clear, version-controlled Bill of Materials (BOM) links the assessed design to what is manufactured. It is essential for demonstrating configuration control, ensuring that each production unit matches the certified design. A generic or uncontrolled BOM undermines the credibility of the entire assessment.

Equally, datasheets for critical components—such as relays, batteries, transformers, and cable glands—are indispensable. These documents provide the rated electrical, thermal, and mechanical limits that underpin compliance. Often, the validity of a protection concept hinges on specific component performance. Missing or ambiguous datasheets can halt the certification process entirely.

Component-level ATEX or IECEx certificates (e.g. for glands, enclosures, barriers) are also vital. They allow the assessor to rely on third-party evaluations rather than re-assessing internal construction. Their absence can force deeper, more time-consuming evaluations at the equipment level.

Better Documentation, Faster Certification High-quality documentation reduces lead times, avoids unnecessary technical queries, and supports ongoing quality assurance, change control, and audit readiness. For manufacturers, investing in documentation early in the development process leads to smoother, more predictable certification outcomes—and ultimately safer, more reliable products in the field.

 Artilcle by Anoop Chandrahasan, ExVeritas Operations Manager

Windows 11 IoT Enterprise LTSC for Arm64: The suitable Microsoft® platform for the IS945.1 tablet in the oil and gas industry

The oil and gas industry places the highest demands on its IT infrastructure. Absolute reliability, long life cycles, minimal energy consumption and strict safety standards are essential. The IS945.1 tablet from i.safe MOBILE has been equipped with Windows 11 IoT Enterprise LTSC for Arm64 to meet precisely these demanding conditions.

Windows 11 IoT Enterprise LTSC for Arm64 is far more than a conventional operating system. This industrial long-term version has been specifically designed for devices that need to operate reliably, securely and continuously for years. The LTSC model (Long-Term Servicing Channel) guarantees up to ten years of support through to October 2034, exclusively with security and quality updates, without disruptive feature updates or forced interface changes. For the IS945.1 tablet, this means stable and predictable system behaviour throughout its entire service life - invaluable in an industry where systems often run around the clock at hard-to-reach or remote locations.

Choosing Windows over alternative platforms means bridging mobility with desktop-grade performance and enterprise integration. The IS945.1 provides a familiar environment for operators and IT departments, accelerating deployment whilst maintaining robust features such as BitLocker, Hyper-V and Remote Desktop. Maximum application compatibility ensures seamless integration into existing Windows-based IT and security infrastructures, protecting established investments.

Arm-based processors are characterised by extremely low energy consumption, high efficiency, and minimal heat generation, eliminating the need for large battery packs or extensive cooling systems.

This results in a lightweight and compact device with optimal battery runtimes, well suited for shift-based field work.

This design, made possible by high integration of modem, GPU and AI engines in a single system-on-chip, ensures operator friendliness without compromising ruggedness.

Refineries, drilling platforms, and pipeline facilities are classified as hazardous or potentially explosive environments. In these settings, the ATEX and IECEx certifications of the IS945.1 tablet confirm its suitability for safe operation in accordance with stringent regulatory requirements.

Modern oil and gas facilities generate enormous amounts of data. The IS945.1 enables powerful edge computing - local data processing directly at the point of use. This is particularly valuable for real-time monitoring, rapid response to anomalies, predictive maintenance and SCADA control systems. Local processing reduces dependence on cloud connectivity and enables faster, autonomous decisions in the field. The platform supports local AI inference and secure 5G/4G connectivity directly on-device.

As critical infrastructure, the oil and gas industry is a prime target for cyber attacks. Windows IoT Enterprise LTSC offers comprehensive security features such as Secure Boot, TPM support, BitLocker encryption and long-term security patches throughout the entire lifecycle.

The IS945.1 tablet from i.safe MOBILE with Windows 11 IoT Enterprise LTSC for Arm64 combines all features that modern oil and gas operations require: long-term stability, explosion protection, superior energy efficiency, edge computing capabilities and the highest security standards. It represents optimal IT/OT convergence, empowering secure field operations whilst protecting software investments - the ideal solution for digitising critical processes in a future-proof manner.

www.isafe-mobile.com


Why Vacuum Selection Matters in Hazardous Engineering Environments

qp21.jpeg


Dust is present in almost every industrial environment. It may be created by production processes, released during material handling, or left behind during maintenance activities. In many cases it is removed using an industrial vacuum cleaner chosen for availability rather than suitability.

In hazardous engineering environments, that choice is critical. Many industrial dusts are harmful when inhaled and a significant number are combustible. Inadequately specified vacuum equipment can allow fine dust to become airborne again, fail to contain hazardous material, or introduce ignition risks in areas where explosive atmospheres may be present. Instead of controlling risk, the wrong equipment can increase it.

Effective dust control begins with understanding the hazard. What material is being collected, how fine it is, whether it presents a health risk, and whether it has explosive potential all influence the correct vacuum specification. The operating environment is equally important, particularly where ATEX zoned areas exist. Once these factors are understood, the vacuum system, filtration, materials of construction and accessories can be specified to match the real risk rather than assumptions.

Engineering a machine for the hazard

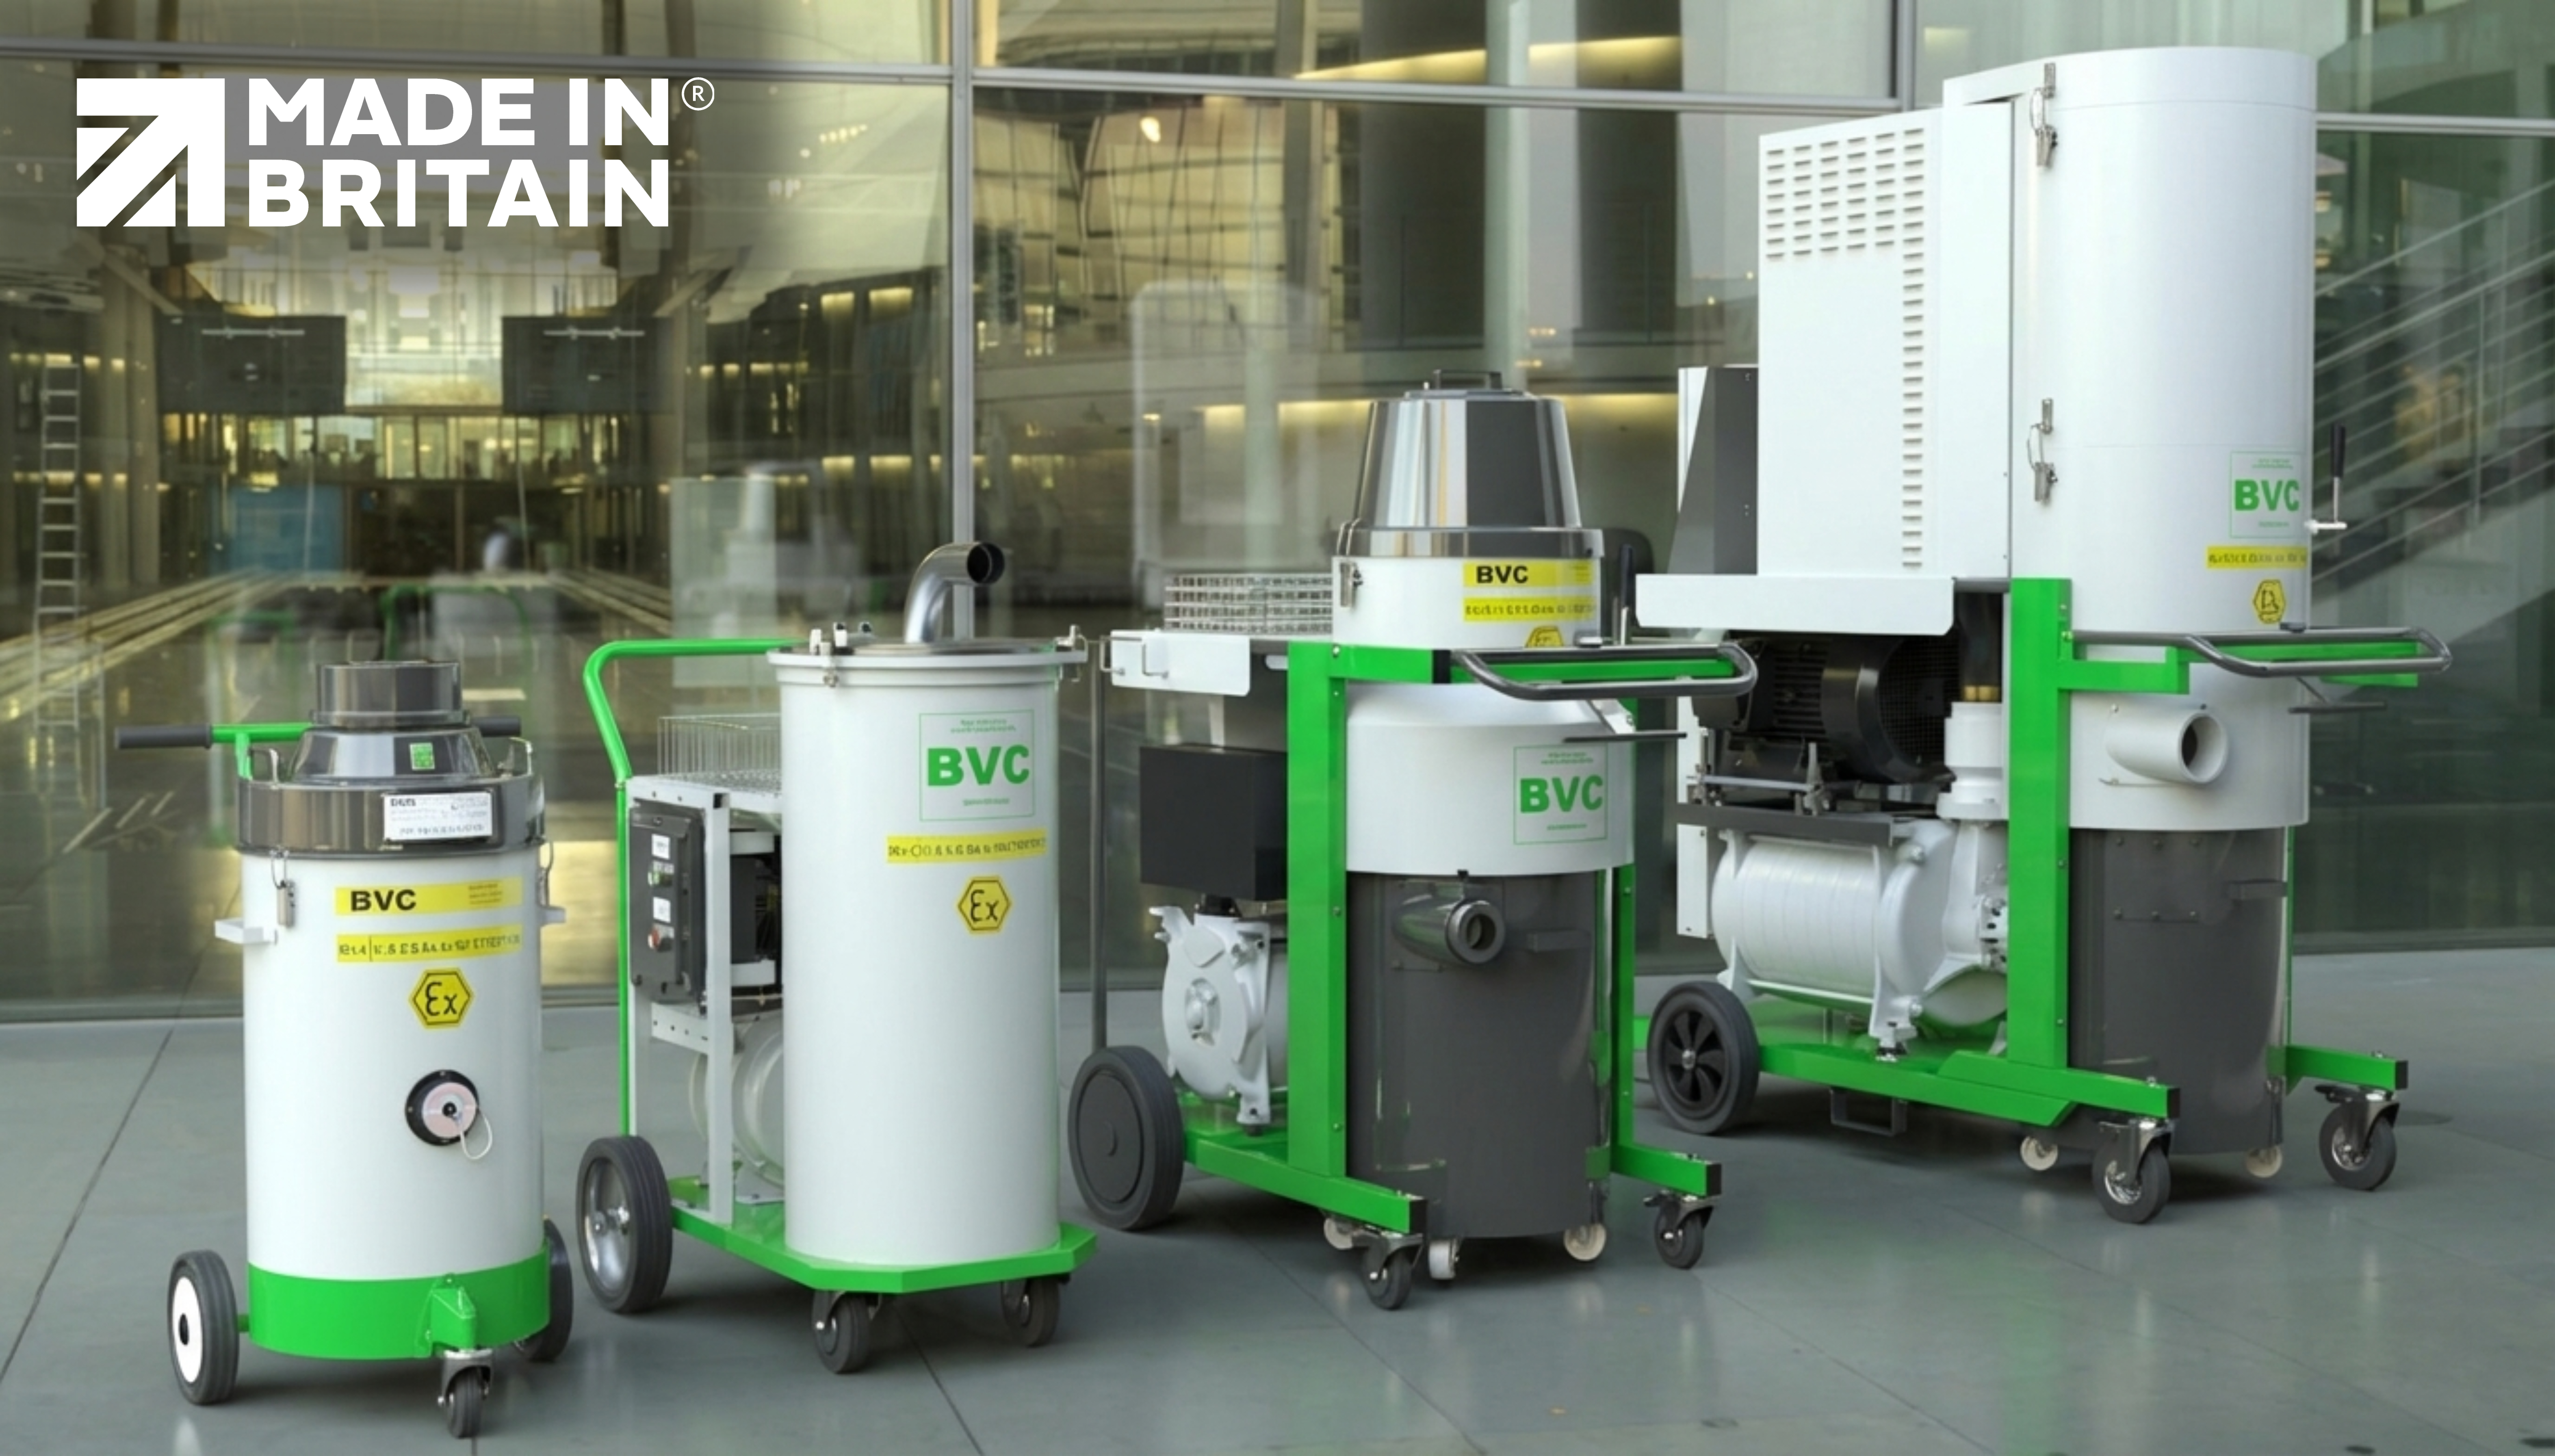
BVC – British Vacuum Cleaners – is built by Quirepace in Fareham and supplied as industrial vacuum systems engineered to order. Rather than relying on a fixed catalogue, machines are sized and configured around the application they will operate in and the hazards they must control.

Where dust is hazardous to health, M-Class or H-Class machines are required. Where an explosive atmosphere may occur, ATEX-rated equipment is essential. In many industrial environments both conditions apply, meaning a single vacuum system may need certification for hazardous dust collection while also being suitable for use in ATEX Dust Zone 21 or 22. Some applications may also require suitability for ATEX gas zones.

Filtration plays a central role in risk control. Anti-static filter media and multi-stage filtration ensure hazardous material remains contained and exhaust air is kept clean, protecting operators and preventing secondary contamination.

Quirepace also engineers application-specific solutions, including systems with low-pressure blown air to dislodge compacted deposits, high-level cleaning tools for structural steelwork and services, and integration with process controls so equipment operates automatically with production.

Systems, tools and long-term value

Correct hose sizing and tool selection improve conveying efficiency, reduce blockages and make cleaning more effective. Portable ATEX vacuums offer flexibility, while larger or higher-risk sites may benefit from Central Vacuum Cleaning systems that remove equipment from hazardous areas and centralise maintenance.

Industrial vacuum systems operate in demanding conditions and are relied upon daily. For this reason, whole-life value, reliability and support are often more important than initial purchase price. Treating vacuum cleaning as part of the engineered hazard control strategy leads to safer operations and more robust long-term performance. 

BVC Quirepace offers free on site demonstrations of BVC equipment at food factories in the UK. For more information or to discuss your site, contact Quirepace:
T: 023 9260 3700
E: This email address is being protected from spambots. You need JavaScript enabled to view it.
W: www.quirepace.co.uk | www.bvc.co.uk

Mention Hazardous Engineering Solutions when you contact us and we will apply a 5% discount to your first order for BVC industrial vacuum equipment.

Oleon Invests in Health and Safety at its Goole Site with support from Tadweld

Oleon, global experts in natural chemistry and sustainable oleochemical production, have invested in class-leading safe tanker access solutions at its Goole facility.


With hundreds of tankers visiting the facility each year, upgrades have delivered improvements to operational efficiency and helped to minimise risk of accidents.

To implement the solution, Oleon appointed Yorkshire based steel fabricators Tadweld Limited, who offer a range of specialist tanker access solutions under their AJAX safe access brand.

Oleon Safety Access

At the James Street site in Goole, Tadweld have installed a full gantry system combined with a Pneumatic Ajax Step Unit, providing safe, permanent access to tankers with enhanced usability and safety. 

Oleon Mobile Step Unit

At Oleon’s New Potter Grange Road site, Tadweld have delivered a set of the company’s mobile tanker access steps, offering a compact, flexible access system that can be easily manoeuvred.

Andrew Akins, Health and Safety Manager said:

“Tadweld understood our access challenges and delivered tailored solutions for each site. Both solutions have improved safety and efficiency. The whole process was seamless and professional. From the initial project meeting, design and solution development, Tadweld understood our desire to achieve best practice for our team and delivered a solution that works for us. We wouldn't hesitate to recommend them.”

Chris Houston, Managing Director at Tadweld, said:

“Ajax tanker access systems have set the industry benchmark for over 40 years. With over 1,000 units installed around the UK, we’re proud that Oleon chose Tadweld to achieve their health and safety objectives”

“Working with Oleon has been a great example of how collaboration across departments - from safety to logistics - can produce outstanding results,” added Mike Godbert, Business Development Manager at Tadweld.