Find ATEX, IECEx, Explosion Protection & Hazardous Area Content...

News

Parker at SMM 2026: Move Fleets. Advance Missions

Exhibiting its marine & defence portfolio in Hall A3, Booth 412

Parker Hannifin, the global leader in motion and control technologies, will present innovative solutions for the marine industry that provide more sea time and less downtime at SMM 2026 in Hamburg, Germany. Held between 1st and 4th September, the trade fair and conference brings together members of the maritime industry, and visitors will be able to find Parker at its Booth 412 in Hall A3.

Across commercial and defence shipping, Parker helps customers address key operational challenges: reducing energy losses, lowering maintenance requirements, improving equipment reliability, and supporting compliance planning as maritime fuel and regulatory pathways continue to evolve. Parker will showcase technologies and solutions that help improve reliability and support more efficient maritime operations. Some filtration technologies that will be on display include the NFM-100 membrane, used in the production of blanketing nitrogen in explosive environments, the Online Ferrous Wear Meter, for condition monitoring of oil and a range of core marine products including well-known brands like Racor Filters.

Visitors to Parker’s booth can meet with the company’s experts to discuss reducing vessel downtime, improving operational availability, and lowering energy and maintenance costs across critical onboard systems. They can also explore support for shipyard or integrator milestones, reliability improvements in demanding commercial and defence marine environments, compliance readiness, future fuel flexibility, and practical solutions for newbuild, retrofit, modernization, or service requirements.

For more information, please visit the event landing page or navigate directly to the dedicated marine page: Innovative Marine Solutions for Design Engineers | Parker

Kalfresh partners with global bioenergy technology leader WELTEC BIOPOWER to deliver flagship Queensland project

KALFRESH has secured leading international technology partner, WELTEC BIOPOWER, to deliver its landmark bioenergy facility at Kalbar, in South-East Queensland, aligning with one of the world’s most experienced and proven providers of anaerobic digestion technology.

The Queensland-based vegetable business has signed an agreement with the German company to design and build the first stage of the bioenergy facility, which will anchor the new Scenic Rim Agricultural Industrial Precinct. The WELTEC equipment is due to arrive on site in late August, when construction of the first anaerobic digestion (AD) tank will begin.

The partnership marks a significant milestone and will unlock the paddock-to-power potential of Kalfresh’s vertically integrated business, which will turn crop residues, processing offcuts and agricultural waste into several renewable by-products. A by-product, a nutrient-rich digestate, will be returned to farms as a biofertiliser, advancing Kalfresh’s long-term vision of circular agriculture.

Kalfresh CEO, Richard Gorman, said WELTEC BIOPOWER will use its proven stainless-steel tank technology, ensuring durability, corrosion resistance and long operational life. “For us, it was critical to work with a partner that has a track record of delivering reliable, long-term infrastructure,” Mr Gorman said.

“This is proven technology, and we’re building it to last. We have visited many operational bioenergy sites overseas, including those designed and built by WELTEC. They have a reputation for designing efficient, high- quality systems that deliver consistently. “Kalfresh sent a group of Queensland farmers to Germany in April to visit Weltec sites and see the AD technology first-hand.”

WELTEC BIOPOWER was established in 2001 and has planned, delivered and constructed more than 450 specialised stainless steel biogas plants in the US, Japan, Cyprus, the UK and Europe. Dirk Krumdieck, CEO and Head of Sales from WELTEC BIOPOWER, says the agreement reflects the extensive preparatory work and technical planning undertaken by WELTEC and Kalfresh over recent years. „We are excited to be delivering a flagship bioenergy project in Australia that combines Kalfresh’s agricultural innovation with our proven European biogas engineering experience,” Mr Krumdieck said.

The project will be delivered in three stages. The first stage involves the construction of a large digester with a diameter of 31.48 metres and a height of 8.8 metres, along with a digestate storage tank, supported by the newly implemented WELTEC Control system.

It represents a new model for Australian agriculture where farming, food production and energy generation operate side by side in a closed-loop system. At full capacity, the facility could feature 14 digesters which would be capable of producing enough energy to power up to 31,000 homes, or fuel up to 98 million kilometres of truck and bus travel annually. “Recent international events have made it clear there’s a real and immediate need for national fuel and fertiliser security,” said Mr Gorman.

“The introduction of a home-grown, dispatchable source of renewable natural gas to the energy mix comes at an important time. We can help transition Australia’s emitters towards emissions-free operation.“This is a practical, farmer-led solution that works today, and can be repeated in the future in agricultural communities across the country, value-adding what is already produced on-farms.”

The Scenic Rim Agricultural Industrial Precinct will co-locate advanced food manufacturing on a 40-hectare site fronting the Cunningham Highway and approximately one hour from Brisbane. The Precinct will feature 16 serviced lots, including three occupied by Kalfresh, with access to on-site renewable power and circular waste services.

For more information on the project visit the Kalfresh Bioenergy website

https://www.kalfreshbioenergy.com.au/

Assessment Update: UKEX vs ATEX – Understanding the Key Differences

Following the UK's departure from the European Union, manufacturers supplying explosion-protected equipment to both Great Britain and the European Union must ensure they understand the differences between the UKEX and ATEX regulatory frameworks. While the technical standards remain closely aligned, the conformity assessment and product marking requirements differ depending on the destination market.

What is UKEX?

UKEX is the conformity marking required for products placed on the market in Great Britain (England, Scotland and Wales). It applies to equipment and protective systems intended for use in potentially explosive atmospheres under the Equipment and Protective Systems Intended for Use in Potentially Explosive Atmospheres Regulations 2016, as amended following Brexit.

Although UKEX is based on the same essential health and safety requirements as the ATEX Directive, products destined for Great Britain must follow the UK conformity assessment process where applicable.

ATEX Remains in Force in the European Union

Manufacturers supplying equipment to EU member states must continue to comply with the ATEX Directive 2014/34/EU and apply the CE and Ex markings where required.

The technical standards supporting both UKEX and ATEX are largely harmonised with the IEC 60079 series, meaning the engineering requirements remain familiar to manufacturers. However, the administrative route to market differs.

Key Differences

Manufacturers should be aware of several important distinctions:

  • UKEX applies in Great Britain, while ATEX applies across the European Union.
  • Products requiring third-party conformity assessment must use an approved UK body for UKEX certification and an EU Notified Body for ATEX certification.
  • Technical documentation and declarations of conformity must reference the appropriate legislation for the intended market.
  • Separate certificates may be required when placing products on both the GB and EU markets.

Planning for Dual Market Access

Many manufacturers continue to serve customers in both Great Britain and the European Union. Planning certification early can help minimise duplication, reduce costs and avoid delays when launching new explosion-protected equipment.

By understanding the differences between UKEX and ATEX, manufacturers can ensure their products remain compliant while maintaining access to key industrial markets.

Compliance Update: Understanding Japan's JNIOSH Certification Requirements for Explosion-Protected Equipment

For manufacturers of explosion-protected electrical equipment, obtaining ATEX or IECEx certification is often seen as the key to global market access. However, companies looking to supply hazardous area equipment in Japan face an additional regulatory requirement.

Under Japan's Industrial Safety and Health framework, explosion-protected electrical equipment intended for use in hazardous locations must comply with the country's Technical Recommendations issued by the National Institute of Occupational Safety and Health (JNIOSH). In many cases, products require certification against these recommendations before they can be legally placed on the Japanese market.

A Different Route to Compliance

While Japan's technical requirements are closely aligned with the IEC 60079 series used internationally, manufacturers cannot simply rely on existing ATEX or IECEx approvals alone. Certification must demonstrate compliance with the applicable JNIOSH Technical Recommendations, which form the basis of Japan's national approval process for explosion-protected equipment.

The recommendations cover the various recognised methods of explosion protection, including:

  • Flameproof enclosures (Ex d)
  • Increased safety (Ex e)
  • Intrinsic safety (Ex i)
  • Pressurisation (Ex p)
  • Dust ignition protection (Ex t)
  • Non-sparking equipment (Ex n)
  • Optical radiation protection (Ex op)

These guidance documents are regularly updated to reflect developments in international standards while maintaining Japan's specific regulatory requirements.

Why It Matters

Japan remains one of the world's largest industrial economies, with significant investment across:

  • Oil & gas
  • Petrochemicals
  • Chemical processing
  • Pharmaceutical manufacturing
  • Hydrogen technologies
  • Energy generation
  • Advanced manufacturing

For overseas manufacturers, understanding the country's certification pathway early in the product development process can prevent costly delays when entering the market.

Planning for Market Entry

Manufacturers intending to export explosion-protected equipment into Japan should review certification requirements at an early stage. Working with certification specialists familiar with both IECEx/ATEX and JNIOSH requirements can help streamline approval and ensure products meet the necessary technical and quality standards expected by Japanese regulators.

Although many technical principles are harmonised with international standards, Japan's certification process remains distinct, making regulatory planning an important part of any successful market entry strategy.

As hazardous industries continue to expand across Asia, understanding regional certification requirements is becoming increasingly important for manufacturers seeking to operate in global markets.

Stargate Hydrogen Opens Electrolyser Factory Amid Industry Hesitation

Stargate Hydrogen inaugurates its new factory with an exclusive event, attended by Kristen Michal, the Prime Minister of Estonia and Jorgo Chatzimarkakis, CEO of Hydrogen Europe. The facility, dedicated to the production of innovative alkaline electrolysis stacks and systems, positions Stargate Hydrogen as a major industrial player on the green hydrogen landscape.  
 
In the first phase, the new factory can deliver 140 MW of alkaline electrolysers annually, which can be expanded to 1GW+ with minor additional investments. With robust support from European investors and IPCEI status (Important Projects of Common European Interest), Stargate Hydrogen is now well positioned to bring down the cost of green hydrogen and help decarbonize critical sectors including steel, fertilizers, and chemicals. Deliveries from the new factory have already started to the existing customers of the company in the European, Middle Eastern, Turkish and Indian markets.  
 
Stargate Hydrogen’s IPCEI project stands as an outstanding example of how professionally managed public support can catalyse meaningful industrial innovation. Facilities like this and the material innovation undertaken by Stargate are exactly what we need to build the hydrogen economy in Europe, and stay competitive, sustainable, and sovereign in the clean energy transition.” — Jorgo Chatzimarkakis, CEO of Hydrogen Europe. 
 
According to the CEO of Stargate Hydrogen, Marko Virkebau, the company is not opening an empty factory — instead, they have adopted a smart, future-oriented approach of gradually scaling up production with modularity at its core. Rather than burdening taxpayers and shareholders with the costs of an oversized and underutilized plant, Stargate Hydrogen has chosen a brownfield site with a flexible floor plan to ensure the best use of space and avoid large upfront investments.  
 
Marko Virkebau, CEO of Stargate Hydrogen, said: “There are currently several electrolyser gigafactories out there that are standing idle and burning through incredible amounts of capital. We have chosen a different strategy, scaling up modularly to meet the growing demand as it rises and when our next-generation innovations are launched to the market. Currently, our production is fully booked until the end of 2025, and we see increasing demand from our existing customers in Europe and new customers from the Middle East and Asia. “ 
 
The event brought together prominent policymakers, industry pioneers, and international partners. Held in the company’s production hall, the event’s main stage was surrounded by products in ongoing assembly, for example the turn-key electrolyser system destined for Fortum and several stacks ready for delivery. 
In times when many companies are scaling down, or even ending their operations, Stargate Hydrogen goes against the tide and is expanding its operations via a gradual and financially sustainable scale-up strategy. 
 
About Stargate Hydrogen: Stargate Hydrogen was founded in 2021 to make green hydrogen affordable for hard-to-decarbonise industries like steel, fertilisers, and chemicals. The company’s focus: improve electrolyser efficiency and cut costs using novel ceramic catalysts and patented stack design.  
With €50M+ in funding from strong investors and IPCEI status, Stargate is scaling production to 140 MW annually. Their list of customers includes Fortum, Utilitas, ABB, Rockfin, and others across Europe, Türkiye and India. 

Stargate Hydrogen signs the first partnership in the UK with Seacht Group.

Agreement marks the company’s entry into the UK hydrogen marketStargate Hydrogen today announced a partnership with Seacht Group, marking its first partnership in the United Kingdom. The agreement is a key step in Stargate Hydrogen’s expansion into the UK and signals the start of its business development efforts in the region.
 
The collaboration brings together Stargate Hydrogen, a European developer of ceramic-based electrolysis technology, and Seacht Group, a UK-based energy and engineering group. Together, the companies aim to gain market share of the green hydrogen projects across the UK, a market with growing demand for low-carbon energy solutions.
 
The partnership will make its first public appearance at the Hydrogen UK Annual Conference & Awards in Birmingham, where companies will jointly engage with industry stakeholders, project developers, and policymakers.
 
“This partnership strengthens Stargate Hydrogen,” said Marko Virkebau, CEO of Stargate Hydrogen: “The UK is a strategic market for us, and we need strong local partners with the experience needed to support project development. This agreement reflects our intention to establish a long-term commercial presence in the UK.”
 
Stargate Hydrogen plans to build on this first agreement by forming strategic alliances with engineering companies and EPC-s in the UK in the coming years, as part of its wider European growth strategy. They see the UK as a market with strong potential for decarbonisation through green hydrogen, particularly across industry and energy systems.
 
“Green hydrogen is expected to play a growing role in the UK’s transition to lower-carbon energy,” said Robert Kelly COO of Seacht Group: “By partnering with Stargate Hydrogen, we are combining advanced electrolysis technology with local market knowledge to help move hydrogen projects forward.”
 
The collaboration supports Stargate Hydrogen’s broader objective of establishing a solid presence across Europe and surrounding regions, while contributing to the UK’s efforts to reduce emissions through scalable green hydrogen production

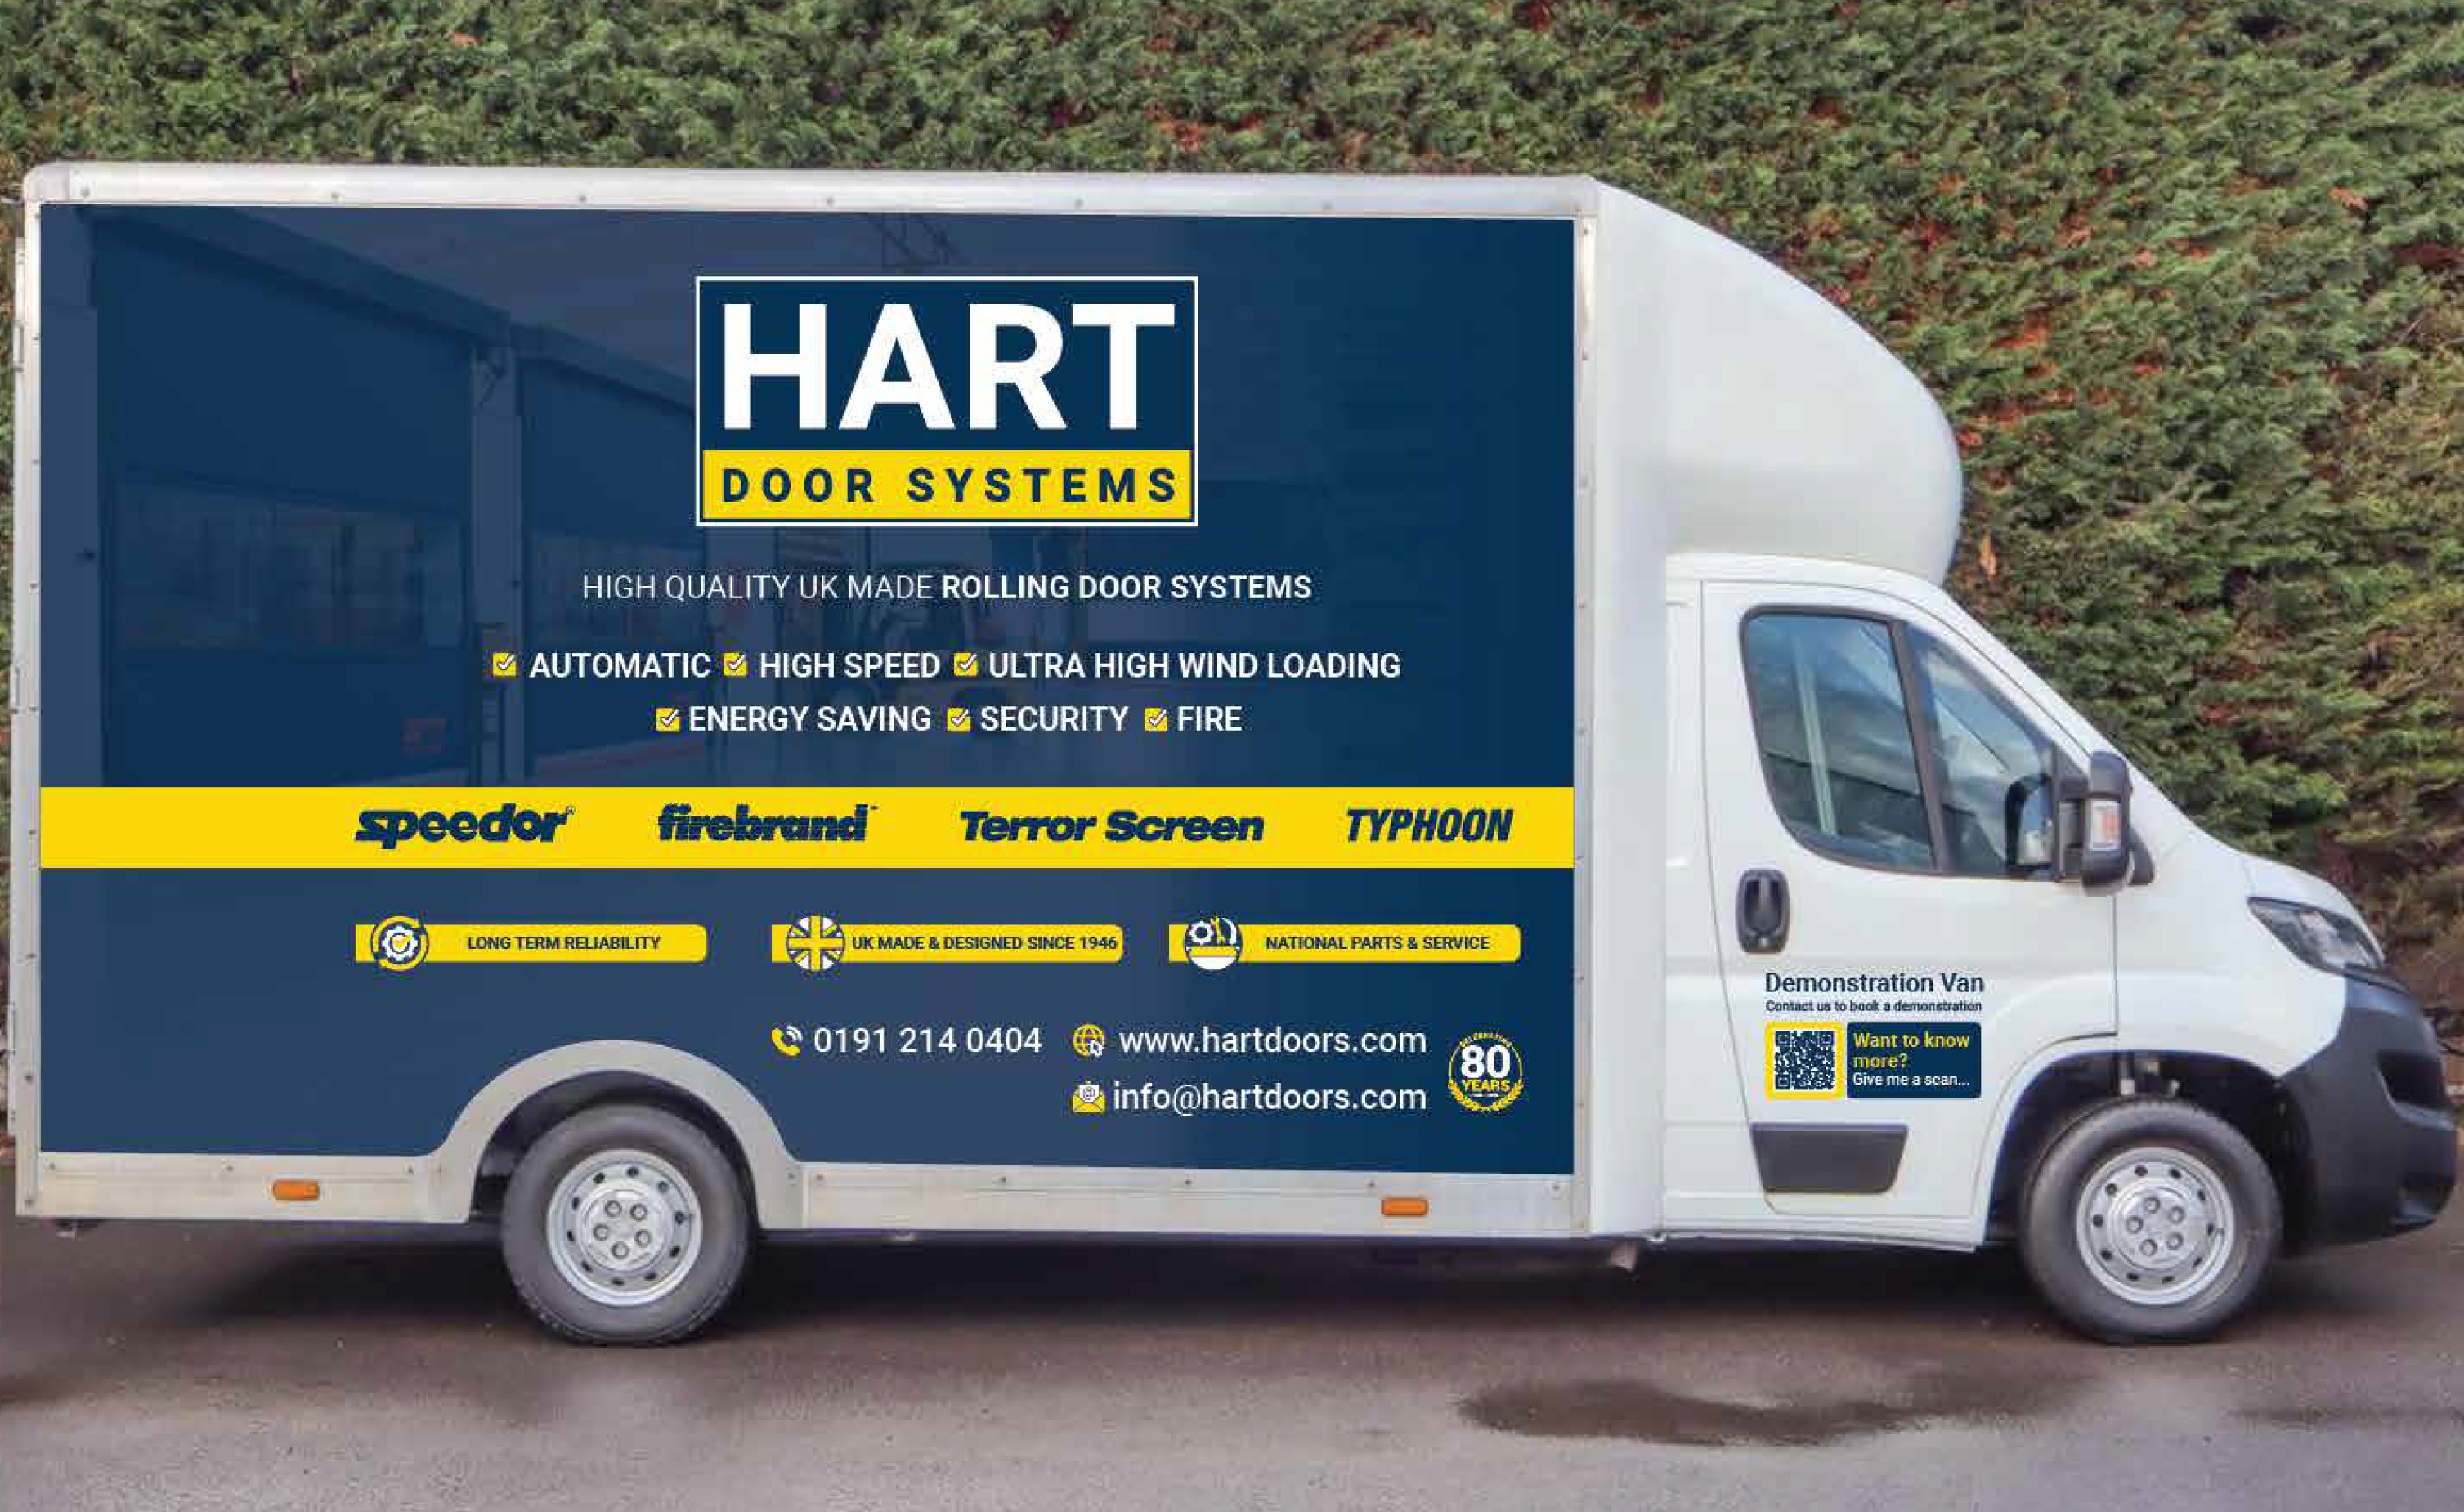
New mobile facility for Hart Doors

Hart Doors, the oldest British manufacturer of industrial high-speed doors and shutters, has invested in a new mobile installation facility.

Chairman Douglas Hart explains: “The focus on the British Isles has been Hart’s very rewarding market but with increasing sales from the north of Scotland to the south of England means a much sharper delivery/installation over a greater geographical area is required. The new facility is outstanding.

“Based in Newcastle UK, we are the most established British manufacturer of high-speed doors and shutters. Founded in 1946, we bring generations of engineering experience and pioneering product expertise to customers worldwide.

“Our innovative products, problem-solving approach and practical experience help companies contain noise, odour and environmental contaminants.

“This spirit of innovation is embedded into our continually evolving product range of Speedor high-speed doorsfire shuttersTerror Screen security rated shutters and specialist doors such as ATEX compliant high-speed doors and shutters,” says Mr Hart.

The installation unit is now operational much to the satisfaction of clients and the installation teams.

www.hartdoors.com

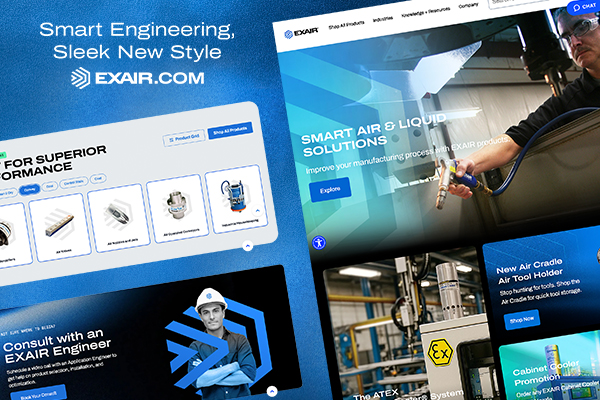
EXAIR Launches Redesigned Website for Enhanced Digital Experience

            EXAIR has unveiled a redesigned website that delivers a more streamlined experience for engineers, maintenance professionals, and manufacturers searching for compressed air solutions. Featuring a modern look that reflects EXAIR's updated brand identity, the new website makes it easier than ever to explore products, learn about applications, and find the right solution for virtually any industrial challenge. Built with performance and usability in mind, the site offers faster page loads, improved navigation, and a cleaner interface.

            The redesigned website introduces several customer-focused enhancements that simplify the buying process from research to checkout. A streamlined shopping experience reduces the number of steps required to purchase products, allowing customers to move from product selection to checkout more quickly than ever before. Visitors can also browse new industry-specific pages featuring relevant product recommendations, application examples, and educational resources, making it easier for users to discover solutions designed specifically for their manufacturing environment. The site also offers ample opportunities to connect with EXAIR through catalog requests, newsletter signups, or speaking directly with Application Engineers to get answers for case-by-case manufacturing dilemmas.

            EXAIR.com reinforces EXAIR's commitment to providing customers with the tools and resources needed to solve industrial challenges efficiently. In addition, visitors have access to the application database, videos, CAD models, blogs, an extensive Knowledge Base, and direct support from EXAIR's Application Engineers. Combined with enhanced site performance and an improved user experience, the redesigned website makes finding, selecting, and purchasing EXAIR solutions easier than ever. https://exair.co/190-newsite

From Operational Data to Explosion Risk Intelligence

Industrial organisations generate a massive amount of information about how risk is identified, managed and controlled, from DSEAR and ATEX assessments and hazardous area classifications to inspection findings, maintenance activity, equipment records, management of change and operational procedures. Most of this information is considered independently and often represents conditions at a particular point in time.
 
EXPAS was founded to address this gap by transforming engineering evidence and operational data into a transparent view of explosion risk and how that risk may be changing.
Central to the EXPAS approach is operational control. Rather than focusing solely on whether assessments, safeguards and systems exist, it considers the factors that determine whether those controls can continue to be relied upon in practice.
 
A critical safeguard may have been correctly specified and installed, but its effectiveness over time can be influenced by maintenance activity, equipment condition, inspection findings, outstanding actions and the operational behaviours and management systems that support it. Individually, these are separate pieces of information. Considered collectively, they can provide valuable signals about the underlying condition of the risk and where weaknesses may be developing. EXPAS structure this evidence across four connected dimensions: Ignition Exposure, Control Fragility, Escalation Potential and Risk Trajectory.
 
Ignition Exposure considers the conditions and operational factors influencing exposure to credible ignition sources, while Control Fragility examines the resilience of the engineering and operational controls relied upon to prevent or mitigate an event. This moves the focus beyond simply confirming that a control exists, towards understanding how effectively it is being maintained, managed and supported operationally.
 
Escalation Potential considers how an initial event could develop if prevention or mitigation measures were unsuccessful, providing greater visibility of the pathways through which an incident could escalate into a more significant explosion, fire, business interruption or loss.
Bringing these signals together over time creates Risk Trajectory, providing a view of whether the underlying risk position is stable, improving or deteriorating as operational conditions and evidence change.
 
Transparency is fundamental to the approach. Rather than producing a black box score, the intelligence remains traceable to the engineering evidence and operational information supporting it, allowing users to understand what is influencing the risk position and where attention may be required.
EXPAS is not intended to replace established DSEAR, ATEX, engineering assessment or inspection processes.
 
Instead, it builds upon them by connecting information that has traditionally existed across separate documents, systems and operational activities.
 
For industrial operators, this can provide earlier visibility of emerging weaknesses and stronger evidence of how explosion risk is being controlled. For insurers and risk engineers, it can provide a more consistent and transparent understanding of the operational factors influencing the underlying risk.
Knowing that a control exists is only part of the picture.
 
Understanding whether it can still be relied upon, what could happen if it fails and which direction the risk is moving provides a much deeper view of risk.
 
That is the shift from static assessment to Explosion Risk Intelligence.
 
Author 
Mike Brimble
 

5 health and safety myths that still put maintenance teams at risk

uvex manufacturing ACTION 03

PPE has come a long way in recent years. Today's products are lighter, more comfortable and more technically advanced than ever before, yet many maintenance and manufacturing businesses still make decisions based on outdated assumptions.

Here, Clair Weston, Head of Marketing at uvex, highlights five common health and safety myths that could be putting maintenance teams at unnecessary risk.

1. "The more hearing protection, the better."

Many people assume that choosing hearing protection with the highest attenuation offers the greatest level of safety. However, overprotection can create its own risks.

If hearing protection reduces noise too much, workers may struggle to communicate with colleagues, hear warning alarms or approaching vehicles. In busy maintenance environments, where communication is essential, this can increase the risk of accidents.

The Health and Safety Executive (HSE) advises employers to select hearing protection that reduces noise to a safe level while avoiding unnecessary overprotection.

Best practice: Carry out suitable noise assessments and choose hearing protection that matches the actual noise exposure rather than simply selecting the highest SNR rating.

2. "Impact protection gloves are too bulky for maintenance work."

Impact-resistant gloves have traditionally been associated with reduced dexterity, but glove technology has advanced significantly.

Modern impact gloves combine lightweight liners, flexible impact protection and excellent grip with high levels of cut resistance, allowing technicians to protect against knocks and crush injuries while maintaining precision.

Best practice: Choose gloves such as the new uvex Hexarmor Helix® 3014IMP that balance protection with flexibility and dexterity. PPE only protects workers if they're willing to wear it consistently.

3. "Clear lenses are suitable for every job."

Many organisations issue clear safety spectacles as standard without considering whether they're the best option for different environments.

Lens colour can greatly affect visibility, comfort and fatigue. Grey lenses help reduce glare outdoors, amber lenses improve contrast in lower-light conditions, while indoor/outdoor lenses suit employees regularly moving between inside and outside.

Best practice: Match lens technology to the working environment rather than automatically specifying clear lenses for every application. For more information, see uvex’s lens tinting advisor.

4. "Safety footwear has to be uncomfortable."

Many workers still accept sore feet and fatigue as simply part of wearing safety boots, but modern safety footwear has changed dramatically.

Lightweight materials, ergonomic sole designs and cushioning technologies help reduce fatigue throughout the working day, improving both comfort and performance.

Best practice: Treat safety footwear as performance equipment as well as protective equipment, considering comfort and support alongside safety certification.

5. "One size fits all."

One of the most overlooked aspects of PPE is achieving the correct fit. Equipment that is too loose, too tight or poorly adjusted is less likely to provide the protection it was designed to deliver.

Poorly fitting gloves reduce dexterity, eyewear that slips is often removed, and hearing protection that doesn't seal correctly may not provide adequate protection. As today's workforce becomes increasingly diverse, a one-size-fits-all approach is no longer appropriate.

Best practice: Offer PPE in a range of sizes and ensure workers are properly fitted. Well-fitting equipment is more likely to be worn correctly, improving both protection and compliance.

Rethinking PPE selection

Maintenance professionals encounter a wide range of hazards throughout the working day. Selecting the right PPE isn't simply about meeting legislative requirements, it's about providing equipment that workers will wear correctly and consistently.

By challenging outdated assumptions around hearing protection, hand protection, eyewear, safety footwear and PPE fit, organisations can improve compliance while helping to create safer, more productive workplaces.

www.uvex-safety.co.uk