Find ATEX, IECEx, Explosion Protection & Hazardous Area Content...

Latest Case Studies & White Papers

Polymeric Leading Edge Protection Extends Lifespan of 42 Wind Turbine Blades

b1.jpeg

Figure 1. Leading edge protection of wind turbine blade using polymeric technology

                                                                                                                                                                                               
In order to achieve net-zero by 2050, according to a 2023 Report from the world-leading authority on climate science, Climate Action Tracker: ‘wind and solar sources in electricity generation will need to reach 57 - 78 percent by 2030, and 79 - 96 percent by 2050.’ In 2022, this figure sat at 12 percent. Needless to say, a colossal scale-up of these industries is anticipated over the upcoming decades.

b2.jpeg

Figure 2. Historical progress toward 2030, 2040 and 2050 targets for share of wind and solar sources in electricity generation (Source: State of Climate Action 2023)

Polymeric Technology Supports Transition to 79 – 96% Renewable Energy by 2050

Given the important role wind power plays in the transition to net zero, it is absolutely critical that windfarms are maintained to an excellent standard. Otherwise, damaged wind power assets may needlessly be decommissioned and replaced; the process of which comes with a hefty carbon footprint as well as considerable financial expenditure.

As such, asset owners are investing in a simple yet extremely beneficial (both from a cost and environmental perspective) solution to extend the lifespan of wind turbines. This solution involves the use of polymeric repair composites and high-performance protective coatings to repair and protect key assets in the wind industry. This includes: turbine blades, nacelles and generating components, turbine bases, towers, transformers, amongst other assets.

The use of this technology is based on a circular economic business model: repairing damaged assets rather than replacing them. In turn, not only does this mitigate the carbon footprint incurred during the replacement process, but it is also enables the asset owner to make significant financial savings as well.

Case Study: 42 Wind Turbine Blades Repaired and Protected

At an onshore Windfarm in Denmark, 42 wind turbine blades were exhibiting signs of severe erosion on the leading edges. Previously, the Customer had used pre-formed shells that were bonded onto the substrate to provide leading edge protection. However, this process proved to be extremely time-consuming and expensive. Therefore, the Customer was seeking an alternative solution which would be financially viable and also ensure optimal operation for many years to come.

b3.jpeg

Figure 3. Damaged wind turbine leading edge


Specification of Polymeric Leading Edge Protection System

Based on test results, the ease of application as well as the high-quality finish that can be achieved, the Customer decided to repair and protect the leading edges with a combination of Belzona 5711 and Belzona 5721.

The thixotropic paste, Belzona 5711 is specially designed to be applied in conjunction with the Belzona 5721 protective coating. This solvent-free LEP system is formulated for the in-situ repair and rebuilding of leading edge erosion and impact damage on wind turbine blades.

Simple Application Method

Commenting on the application process, Morten Sivertsen, General Manager at AESSEAL Danmark A/S said: “Surface preparation was carried out on each of the 42 blades, followed by the direct application of 90 kg (198.4 lbs) of Belzona 5711 from self-mixing cartridges onto the blade. The repair area was then contoured using a piece of Belzona mixing board. Once cured, a visual inspection was conducted to ensure the application’s readiness for overcoating with 144 kg (317.5 lbs) of Belzona 5721. Using a short-bristled brush, this system was then applied to the leading edge and left to cure for 30 – 60 minutes. With three rope access technicians carrying out the applications, on average, six – nine turbine blades were completed each day.”

b5.jpeg

Figure 5. Morten Sivertsen, General Manager at AESSEAL Danmark A/S


In-Situ Repair Ensured Minimum Downtime Was Incurred

As the polymeric systems were applied in situ without the need for specialist tools or equipment, this ensured that a fast and seamless application was carried out. Thus, this enabled the Customer to make considerable financial savings as it mitigated the profit loss that can be incurred through lengthy periods of downtime.

b6.jpeg

 Figure 6. Leading edge repaired and protected with Belzona 5711 and Belzona 5721


Safeguarding Key Wind Power Assets for the Long Term  


The scaling up of the wind power industry is absolutely critical in order to support the transition to renewable energy, in keeping with the net zero by 2050 pathway. By safeguarding key assets within this industry through the use of polymeric technology, asset owners can successfully bypass the environmental and financial costs associated with asset replacement. Therefore, it could be argued that polymeric technology plays an intrinsic role in supporting this energy transition. 


About AESSEAL DANMARK A/S:


AESSEAL DANMARK A/S is a subsidiary owned by AESSEAL Plc and is the authorised Belzona Distributor for the Denmark territory. Established in 1999, AESSEAL DANMARK A/S provide industrial repair composites and protective coatings to a variety of industries including petrochemical, mining, power, sugar, pulp and paper, amongst others.  

Please click on the following link for more information about AESSEAL DANMARK A/S.

Electric hoist leaves large distillery in high spirits

The world’s largest producer of spirits is now benefiting from a turnkey package of three Italkrane ATEX-rated electric chain hoists supplied by Hoist & Winch Ltd. Operational within a new extension of the Scotland-based distillery, the 2-ton swl (safe working load) hoists raise and lower sealed vessel lids and baskets containing raw materials used in the production of gin.

Among the challenges of this demanding project was a restriction in the overall height of the new building due to local planning laws. In turn, only limited headroom is available for lifting operations over the vessels. Critical for the application, therefore, was the specification by Hoist & Winch of Italkrane YY series electric chain hoists featuring a low-headroom design. The ATEX specification of the hoists is necessary due to the vapours and fumes produced in the manufacture of alcohol-based products.

Italkrane YY series electric chain hoists feature an Ex d electrical enclosure design to contain any explosions and stop flames, sparks and hot gases from escaping. Full anti-spark features are in place for all components subject to sliding friction, including the brass trolley wheels. Also present is a non-sparking load hook, brass anti-tip device and polycarbonate pendant control ensuring explosion protection up to Zone 1 II B T4 classification.

The power supply to each hoist unit is via a festoon cable track system complete with sliding trolleys and support arms clipped to the top flange of the hoist runway beam. Each hoist unit also features an Italkrane heavy-duty geared top/bottom limit switch and friction-type slipping clutch overload protection device.


“Although we provide a full spectrum of lifting equipment services, Hoist & Winch is particularly at home supplying equipment for demanding industries, including the distillery sector,” explains Hoist & Winch Director Andy Allen. “We have extensive knowledge of this industry, where our quality of service and flexible approach ensure the highest levels of customer satisfaction.”

Due to the critical nature of the project and the risk of explosion throughout the high-risk site, it was clear that very stringent planning and close monitoring of working practices would be necessary at all times. In addition, the site work was subject to Construction Design and Management (CDM) Regulations, supported by a requirement for all site engineers to hold a valid CCNSG Safety Passport/CSCS competency certification.

Installation took place over seven days, with a Hoist & Winch CompEX-certified electrical installation engineer completing all connection work. The load testing of each hoist unit and complete runway beam took place using a dynamic test load of 2t + 125% proof load. Additional functional testing using the vessel lids and raw material baskets proved system functionality in line with customer requirements.

Following the issue of a LOLER (Lifting Operations and Lifting Equipment Regulations) Thorough Examination Report for all installation work, Hoist & Winch provided on-site training for the distillery’s operating personnel.

Although providing the optimal solution for this large distillery, Italkrane ATEX-rated electric chain hoists are also suitable for many other applications requiring safe lifting operations in explosion risk environments. In addition, Hoist & Winch can offer ATEX wire rope hoists for longer lifting tasks, heavier loads up to 50t swl and higher duty applications.

Visit www.hoistandwinch.co.uk for further information and to view recent case studies.

Heavily Corroded 872 Metre Oil Pipeline Restored with Composite Wrap

An underground oil pipeline at a Refinery in Spain was suffering from severe corrosion. If left unchecked, the pipeline, 872 metres (2860.8 ft) in length, would have incurred severe metal loss. As a result, disastrous consequences, both financially and also from an environmental perspective, would have ensued.


Figure 1. Corroded pipeline restored with composite wrap

fig_1_Aug.jpeg

Solution Sought to Mitigate Cost and Carbon Footprint of Pipeline Replacement   

A prompt repair was required for the carbon steel pipeline, 55.9 cm (22 inches) in diameter, in order to mitigate any further corrosion damage being incurred. In fact, if left unchecked, this would have caused the substrate to completely corrode through and, therefore, serious environmental issues would have ensued.  

A potential solution would have been to completely replace the pipeline. However, considering its mammoth length, this process would have required considerable financial expenditure and, furthermore, would incur a hefty carbon footprint.

For every ton of steel that is produced, 1.85 tons of CO₂ - nearly double the amount - is released back into the atmosphere (Carbon Clean). In addition to this, the process of removing and disposing of the damaged pipeline further ratchets up the carbon footprint of this process.

As well as the environmental impact of replacing the corroded pipeline, this process would also require a considerable period of downtime which would lead to further profit-loss. The combination of these factors, costly in both a financial and environmental sense, led the Customer to seek out an alternative solution to replacing the steel pipeline.  

Expensive Replacement Process Bypassed with Composite Wrap

The Customer decided to repair and protect the pipeline with a combination of polymeric technology in order to bypass the drawbacks associated with replacing the pipeline.

The following systems were specified and applied following an inspection from Elena Expósito Fernández, AMPP (NACE) Certified Coating Inspector Level 2 and Technical-Commercial Delegate at authorised Belzona Distributorship Rodator Composites:  

“The 2-part epoxy paste, Belzona 1111 (Super Metal), was specified to fill in any gaps in the weld seams to ensure the pipeline had a smooth profile. For heavily corroded areas, plate bonding was required using steel plates which were 50 cm x 60 cm (19.9 in x 23.6 in) in size, with a thickness of 5 mm (0.2 in). These were bonded into place using the epoxy structural adhesive, Belzona 7311. To reinforce the pipeline, the composite wrap, Belzona SuperWrap II, was specified. Finally, the anti-corrosion coating, Belzona 5811 (Immersion Grade), was chosen to provide long-term corrosion protection.”   


Figure 2. Elena Expósito Fernández, Technical-Commercial Delegate at Rodator Composites

fig_2_Aug.jpeg


Figure 3. Application of composite wrap, Belzona SuperWrap II, to the steel pipeline

fig4.jpeg


Figure 4. Anti-corrosion coating, Belzona 5811 (Immersion Grade), applied to pipeline

fig3.jpeg

Polymeric Technology Supports Decarbonisation of Oil and Gas Industry    

The Customer was able to successfully bypass the drawbacks associated with complete pipeline replacement by instead, opting to repair and protect the pipeline with a combination of polymeric technology. As well as making huge financial savings, this solution enabled the Customer to also minimise its environmental impact as well.

As the oil and gas industry continues to decarbonise, this latter point is particularly paramount. Polymeric technology is an extremely viable way in which oil and gas asset managers can make great strides in mitigating the carbon footprint of their facilities. An increased uptake in the use of cold-applied repair composites and protective coatings would help to accelerate the decarbonisation of this industry.

For more information, visit: www.belzona.com

Ensuring Safety in Hazardous Environments: A Case Study on ATEX Safety Showers

In industries where flammable gases, vapours, and dust are present, ensuring the safety of employees is of paramount importance. The European Union's ATEX Directive 2014/34/EU, aim to regulate equipment used in potentially explosive atmospheres, requiring companies to implement safety measures that mitigate the risk of ignition and protect personnel. This blog examines a company's implementation of ATEX safety showers to enhance workplace safety and meet regulatory compliance.

All chemical manufacturing facilities that handle or specialise in the production of volatile chemicals, it is imperative to adhere to ATEX regulations to protect employees from potential hazards. One of the key aspects of ATEX compliance is the provision of safety equipment, including safety showers and eye wash stations, to ensure the safety of workers in the event of chemical spills or exposure.

The Challenge and Solution

Compliance with ATEX Regulations: The company needs to comply with ATEX Directive 2014/34/EU, which required the implementation of safety measures to prevent explosions in areas with potentially explosive atmospheres. This includes providing ATEX-compliant safety showers.

Employee Safety: The safety of employees working with volatile chemicals is a top priority. You need to ensure rapid and effective decontamination in case of chemical exposure.

Equipment Selection: Choosing the right ATEX-compliant safety showers is essential.  You must evaluate the specific requirements of your facility, including location, potential hazard levels, and the number of showers needed.

 This is something Aqua Safety Showers can help with.  We manufacture a full range of safety showers designed to meet the specific needs of sites and provide optimal protection.

Get peace of mind knowing that safety showers from Aqua Safety Showers will be manufactured from corrosion resistant materials and come with a two-year warranty, further promoting a safety-conscious workplace culture.

www.aqua-safety.com


High-Performance Coating Protects Tanks at Biopolymer Production Plant

At a chitosan production plant in Scotland, UK, a high-performance, anti-corrosion coating was used to coat the internal lining of three tanks, protecting them against aggressive, acidic substances for the long term. Given the important role the tanks play in the process of turning large amounts of shellfish byproduct into the biopolymer chitosan, it was imperative that these assets were safeguarded against future damage with the use of a high-performance coating.

m1.jpeg
Figure 1. High-performance coating required to protect tanks against corrosion

Production of Biopolymer from Shellfish Shell Byproduct

CuanTec has created a circular economic business model designed to mitigate the carbon footprint created from the unnecessary disposal of unused shell within the shellfish industry and converting it into valuable chitosan products.

Indeed, the carbon footprint of food waste is staggering. According to data from the UN, food waste contributes to 8% of global greenhouse gas emissions. This means that if food waste was a country, it would be the third-largest emitting country in the world.

At COP28, negotiators from 200 Parties agreed on the science from the Intergovernmental Panel on Climate Change (IPCC) that global greenhouse gas emissions need to ‘be reduced by 43% by 2030’, in order to limit warming to 1.5°C (2.7°F) by 2050, in line with the Paris Agreement. With this in mind, circular business models such as that offered by CuanTec, play an important role in mitigating carbon footprints and limiting global warming to 1.5°C (2.7°F).

Safeguarding Key Assets

Considering the important role businesses such as CuanTec play in this decarbonisation and upcycling journey, it is absolutely fundamental that key assets within these types of businesses, such as machinery, equipment, buildings and structures, are safeguarded to an excellent standard. Otherwise, damage and wear can jeopardise the integrity of assets, and therefore this can undermine the environmental benefits these types of business models offer.

For example, the carbon footprint of steel is phenomenal: for every tonne of steel produced, nearly double the amount of carbon dioxide (CO2) is released back into the atmosphere. Therefore, if a steel asset becomes damaged, not only can this lead to costly replacement fees, but this process can also incur a hefty carbon footprint as well.

As such, numerous industries invest in industrial repair composites and high-performance coatings in order to bypass this replacement process. In this way, polymeric technology mirrors the circular economic model of businesses like CuanTec, as this technology can repair, protect and even intrinsically improve assets that would otherwise be decommissioned and sent to landfill. Thus, it could be argued that polymeric technology has a critical part to play in the decarbonisation of multiple sectors, supporting a net zero by 2050 pathway.  

Pre-Used Tanks in Need of Rigorous Corrosion Mitigation Measures  

CuanTec wanted to deploy three steel tanks in their process of turning shellfish shell into high quality, traceable chitosan products, made to the exacting technical specifications of their customers. The tanks had already been in use elsewhere, but were otherwise still in good condition. In order to ensure the tanks were capable of withstanding the harsh chemicals they would come into contact with, the Customer decided to invest in some polymeric technology to protect them.

System Specification: High Performance Coating, Belzona 1391T

Following an inspection from Clive Leadbitter, Senior Field Sales Engineer at authorised Belzona Distributorship, Belzona UK, the high-performance coating, Belzona 1391T, was specified. As this system is capable of protecting assets against corrosion in extremely aggressive and acidic environments, this was the ideal solution for the steel substrate for this specific application.

In addition, as Belzona 1391T can be applied in situ without the need for hot work, this would ensure that the application was carried out as quickly as possible, whilst minimising the health and safety risks that can arise when hot work is involved.

Belzona 1391T has undergone direct food contact (FDA) testing, the results can be found here.

m2.jpeg

Figure 2. Tank used in process of creating biopolymer, chitosan

Application Procedure

Commenting on the application procedure, Clive said: “Surface preparation was carried out by grit-blasting. Following this, using a stiff-bristled brush, two coats of Belzona 1391T were applied at a thickness of 450 µm (17.72 mil) per coat. Once the application had cured within the space of 24 hours, the application was complete.”

m3.jpeg

Figure 3. Application of high-performance coating, Belzona 1391T

Polymeric Technology Supports Net Zero by 2050 Pathway

Considering the important role businesses like CuanTec play in carbon mitigation, it is absolutely critical that key assets are protected for the long term against damage such as erosion and corrosion. As such, polymeric technology plays an important part in safeguarding these assets, and therefore contributing to the net zero by 2050 pathway.  

www.belzona.co.uk

Belzona 5811DW2 (DW Immersion Grade) Approved by Flour Mill for Dry Food Contact

Introduction:

In the pursuit of maintaining high standards of safety in the food and drink Industry Belzona is constantly seeking innovative solutions to address challenges related to equipment maintenance and corrosion protection. Recently, after undergoing rigorous tests to ensure its suitability for dry food contact, a breakthrough has been achieved with the successful application of Belzona 5811DW2 (DW Immersion Grade), a cutting-edge protection system, in a Flour Mill in Belgium.

Understanding the Need for Food-Safe Coatings:

The food and drink industry is bound by strict regulations and guidelines to ensure the safety and quality of products. Food comes into contact with many materials and articles during its production, processing, storage, preparation and serving, before its eventual consumption. The European Food Safety Authority state that Food Contact Materials (FCMs) should be sufficiently inert so that their constituents neither adversely affect consumer health nor influence the quality of the food.

Flour mills, being a crucial part of the food supply chain, must adhere to these standards. Equipment used in the milling process, such as storage tanks, hoppers, chutes, and conveyors, is prone to wear, corrosion, and degradation over time. Traditional coating solutions often fall short in providing a long-lasting, food-safe barrier.

What is the EU Food Regulation 10 2011?

EU food contact legislation covers the general rules applicable to all materials and articles intended to come into contact with foodstuffs (Regulation (EC) No. 1935/2004). For specific materials such as plastics, more detailed legislation has been additionally in place for several years.

Regulation (EU) 10/2011 sets out safety requirements for plastic materials and articles intended to co­­­­me into contact with food. This regulation is a specific measure for plastic food contact materials as mentioned in the European Framework Regulation (EU) 1935/2004.

This Regulation applies not only to plastics food contact packaging but to equipment such as food storage tanks, pipes, pumps, containers, conveyer belts, etc.

Belzona 5811DWII (DW Immersion Grade) Approved for use on Large Storage Tank at a Flour Mill

Belzona 5811DW2 (DW Immersion Grade) is a solvent-free coating initially designed for the protection of surfaces operating under potable water immersion or where potable water approval is required.

Reacting to customer demand, Belzona Distributor; Perspect Benelux recently invested in comprehensive testing to evaluate the coating’s suitability for contact with dry foodstuffs.

Their customer, a large Mill in Belgium who specialise in the production and development of physically treated wheat flour and mixes used as cake flour, sought a coating suitable for contact with flour which would provide long term corrosion protection. Building on the success of achieving WRAS approval for contact with drinking water, Belzona 5811DW2 (DW Immersion Grade) was put forward as a possible solution.

Comprehensive Testing:

Confident in the performance of the Belzona, Perspect Benelux opted to have Belzona 5811DW2 (DW Immersion Grade) tested by the Belgian packaging institute; IBE-BVI, who are an accredited independent laboratory according to ISO 17025, recognised throughout Europe. Their results confirmed the coating’s compliance with specific requirements of European Regulations No. 1935/2004 and No 10/2011 for prolonged contact with dry foodstuffs.

Perspect Benelux was able to provide tailored support to the customer, in collaboration with Belzona, by providing sufficient data and evidence to satisfy the customer that Belzona 5811DW2 (DW Immersion Grade) is safe and suitable for their specific needs and service conditions.

The positive results were recognised on completion of the project, by the FAVV (Federal Agency for the Safety of the Food Chain) who confirmed application was completed according to the approved method, using Belzona 5811DW2 (DW Immersion Grade).

The unique formulation of this Belzona coating not only ensures compliance with food safety regulations but also offers outstanding protection against corrosion and abrasion. It has been certified as non-leaching, with no harmful emissions or influences on dry food products and flour based on this customer’s specification.

This future-proof coating was also found to conform to the maximum limits of mineral oil aromatic hydrocarbons (MOAH), mineral oil saturated hydrocarbons (MOSH) and Polyolefin oligomeric saturated hydrocarbons (POSH).

The likelihood of these guidelines becoming a requirement in the near future is significant due to the new EU Food standards coming in place.

The results of the tests were not only promising but exceeded expectations, leading to the green light for the application to the internals of a 6000 sq. metres (7175.94 sq. yards) in total flour storage tank of 30 tanks.

May_1.jpeg

Original tank substate

may2.jpeg

Due to the age of the installation, the original lining was blistering and there was a risk it could contaminate the product to be stored in the tanks. In order for the customer to re-use these old, out of service tanks, a new lining was required. Other linings were tested, however Belzona 5811DW2 (DW Immersion Grade) was the only one approved by the QA-QC department. The alternative would have been to build a new silo complex which would have been extremely expensive.

Application Process:

The application of Belzona 5811DW2 (DW Immersion Grade) in the Flour Mill followed a meticulous process to ensure long-lasting protection. The steel surfaces of the tank to be coated were prepared, cleaned, and blasted to the recommended standard of cleanliness, Swedish Standard Sa 2½, SSPC-SP10 (Near-White Metal) with a minimum profile of 3 mils (75 microns). Two coats were then applied by airless spray in cream, to a Dry Film Thickness of 400µm (15.75 mil).

may3.jpeg

Blasted surfaces  
 
may4.jpeg
 
may5.jpeg
 
   Completed application of Belzona 5811DW2 (DW Immersion Grade)
 

Benefits of Belzona 5811DW2 (DW Immersion Grade) in Flour Mills:

may6.jpeg

Coated tank internals

Tested in Accordance with Parts of the Food Safety Regulations: Belzona 5811DW2 (DW Immersion Grade) meets some of the stringent requirements for materials in contact with dry foodstuffs, providing a reliable solution for compliance with regulatory standards.

Extended Equipment Lifespan: The robust nature of the lining enhances the durability of equipment, reducing the frequency of maintenance and replacement.

Solvent-Free Formulation:  The lining’s solvent-free formulation means it is not only food-safe but also environmentally friendly. This characteristic aligns with the Belzona’s commitment to sustainable practices, prioritising the safety of both workers and the surrounding environment.

Corrosion Resistance:  Belzona 5811DW2 (DW Immersion Grade) acts as a barrier against corrosion, preventing the degradation of equipment and maintaining equipment integrity.

Improved Operational Efficiency: With reduced downtime for maintenance, flour mills can operate more efficiently, contributing to increased productivity and cost savings.

Future Potential for Food Manufactures:

may7.jpeg

The successful lining of ten tanks (to date) with Belzona 5811DW2 (DW Immersion Grade) in this Flour Mill highlights the potential of this innovative lining being adopted into the maintenance practices of food manufacturers across Europe. As industries evolve, the implementation of such advanced solutions will become pivotal in ensuring a reliable and sustainable food supply chain

How Can Polymeric Solutions Support a More Sustainable Marine Industry?

The marine industry plays an essential role in steering the course of global commerce the total value of the annual world shipping trade has reached more than $14 trillion (US dollars). According to the United Nations (UN), a staggering 90% of everything we consume is transported by sea. Given the colossal size of the marine industry, it is essential to implement a range of strategies to enhance its sustainability. For example, it is imperative to discover a more sustainable fuel source, and finding solutions that enhance energy efficiency will be crucial.

Of these strategies, advanced coatings and repair composites play a significant role, offering not only the promise of efficiency gains and cost savings but also a seamless alignment with the broader goals of the Blue Economy. The UN iterates that the Blue Economy should “promote economic growth [...], while at the same time ensuring environmental sustainability of the oceans and coastal areas”. By simultaneously reducing costs and fortifying assets, these solutions, such as those produced by Belzona, echo these Blue Economy principles, steering the marine industry towards a more sustainable future.

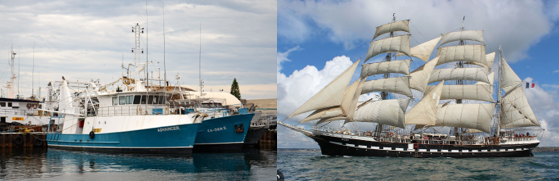
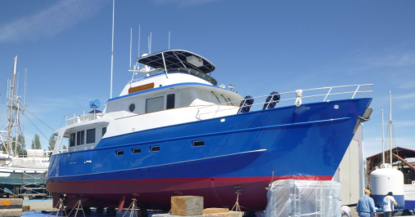
bel_april_1.jpeg

Boats new and old repaired and protected with Belzona

What is the Environmental Impact of the Marine Industry?

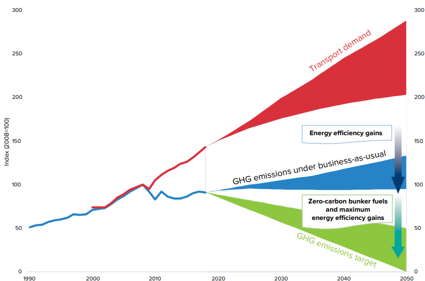
Climate Action Tracker reports that the maritime sector presently accounts for about 3% of all global greenhouse gas (GHG) emissions. If left unregulated, projections suggest that this figure could surge to 17% by 2050. Thus, there is a pressing need for measures to curb and limit this escalation. Surprisingly, Brazil, the 5th largest country in the world, emits just 2.44%, underscoring the maritime sector's outsized role in global emissions.

To contextualise this further, marine transportation far surpasses both the carbon and total greenhouse gas emissions of international aviation. While aviation, a major emitter, contributes about 600 million tonnes of CO2 (MtCO2) per year, marine transport creates a huge 940 MtCO2 annually. Notably, the maritime industry also emits more than twice the amount of total greenhouse gas.

These statistics reveal the mammoth role of shipping in global emissions compared to other industries. Comprehensive measures are urgently needed to address and mitigate the environmental impact of the marine industry in the pursuit of sustainable practices.

What Strategies Are Being Implemented to Address This?

In recent years, a number of new regulations have been created to reduce and prevent air pollution created by shipping. For example, Annex VI of the MARPOL treaty, set in place by the International Maritime Organization's (IMO) limits the sulphur content of marine fuels and regulates emissions of NOx. 

A chapter of this treaty added in 2011 targets operational energy efficiency measures with the goal of diminishing greenhouse gas emissions. There is a growing emphasis on adopting cleaner alternative fuels, improving energy efficiency, and hull design modifications, to reduce the carbon footprint of the industry. In addition, steps are now being taken to minimise the impact of heavy shipping on sea life. Let's take a look at some of these strategies in more detail:

belzona_april_2.jpeg

Efficiency restored with Belzona for bow thruster of private yacht

The Marine Fuel Dilemma

In the pursuit of environmentally sustainable alternatives to Heavy Fuel Oil (HFO) and Marine Gas Oil (MGO), various options, such as LNG, hydrogen, ammonia and methanol, have been explored - each with its own set of challenges.

Liquefied Natural Gas (LNG) has grown in popularity in recent years; however, it is not a viable alternative as switching to LNG would not create a reduction in total GHG emissions. Although LNG has a lower carbon content, it raises methane emissions, which are 80 times more potent than CO2. In fact, the International Council on Clean Transportation (ICCT), asserts that using LNG as a marine fuel emits over 120% more life cycle GHG emissions than MGO. It therefore must be acknowledged that LNG, despite its lower carbon content, remains a high-emission fossil fuel and falls short as a sustainable alternative.

Sustainably produced hydrogen, ammonia and methanol, when produced from renewable sources, are all good sustainable options but face challenges in availability, storage and flashpoint. For example, Hydrogen encounters storage challenges due to volume. Furthermore, most hydrogen produced today is grey hydrogen (not produced sustainably). If enough green hydrogen could be produced and stored it would make a great sustainable alternative. Ammonia boasts easier storage characteristics but would also need to be produced in a carbon-neutral manner and has a low flash point. Provided a sufficient quantity could be produced, green hydrogen, green ammonia or green methanol offer sustainable options. As the industry grapples with the marine fuel dilemma, it becomes evident that more work is required to find a truly sustainable solution to this complex problem.

bel3.jpeg

Historical and projected transport demand and GHG emissions from international Shipping| Source: UNEP, World Bank

Marine Cavitation

Thinking beyond greenhouse gas, the blue economy faces a host of other environmental concerns, including underwater noise pollution. Propeller cavitation leads to excess fuel consumption and can generate as much as 180 decibels of underwater radiated noise (URN) which can be heard by marine life over 100 miles away.

Propeller-induced cavitation is the formation and rapid collapse of bubbles, and this is the main source of underwater sound produced by ships. In fact, the propellor is responsible for about 80% of a ship's URN. The EU has already put in place thresholds to cut down on underwater noise and the IMO issued guidelines last year too. The UN has 17 Sustainable Development Goals and Goal 14, Life Below Water addresses the need to protect marine life. A recent study by the University of Victoria showed how beluga whales avoid marine noise even when many miles away as it masks their vocalisations. This can lead to chronic stress and the animals being displaced from their habitat. Reducing underwater noise footprint will help with species conservation.

Cavitation damage also reduces the propulsion efficiency of a propeller, incurring economic loss due to excessive fuel consumption and the requirements of frequent maintenance. It is clear then a long-term solution for propellor cavitation is required.

Case Study

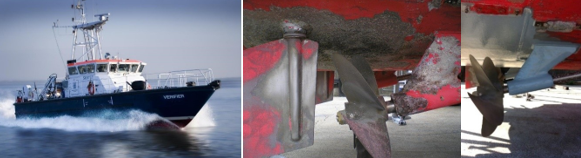
One solution to reduce propellor cavitation, is to repair and protect cavitated propellers with Belzona. In the example below, Belzona 1111 (Super Metal) was used to build up the worst affected areas and then Belzona 1341 (Supermetalglide) was brush applied to provide overall protection. The customer opted for this solution after the failure of welding and inferior coatings. In a study carried out by Leeds University, it was found that Belzona 1341 (Supermetalglide) was fifteen times smoother than polished stainless steel, making it ideal for reducing resistance and noise as well as increasing efficiency. The port now has the confidence to inspect on a less frequent basis meaning the vessel can survey the river for longer periods, saving time and money in a dry dock.

bel4.jpeg

After 10 years of service the hull of the vessel was suffering from cavitation around the propellor area. 

Engine Chocking

As well as repairing and protecting propellors from cavitation, engine chocking to reduce vibrations is key for noise reduction and safety. The essential role of engine chocks is to ensure the proper alignment and stabilisation of ship engines, promoting overall operational reliability.

This is crucial as, left unaddressed, loose bolts can lead to heavy engine vibration, misalignment, bearing damage, and even crankcase explosion. Vibrations may also loosen torque on foundation bolts in crucial components like main engines, turbines, diesel-electric drives, gearboxes, and thrust blocks. Furthermore, if an engine is misaligned or chocks are incorrectly fitted, the overall life span is reduced, and replacement is costly from both an environmental and financial perspective.

Historically, metal has often been used for chocking, however, polymeric resin chocks prove to be a superior alternative. Compounds such as Belzona 7111 (Marine Grade), provide precise alignment with non-shrinking properties and, high impact and high compressive strength, saving time and manpower compared to conventional methods. Specifically designed to endure the physical and thermal shock common to marine environments. This makes it ideal for pouring foundations of heavy ship propulsion systems and other heavy equipment where alignment, and anchorage are essential.

Approved by the American Bureau of Shipping and Lloyd’s Register Classification, Belzona 7111 (Marine Grade) assures lasting alignment and durability, underscoring its excellence in ensuring safety and longevity in maritime applications. Minimising marine noise and extending asset life through solutions, such as those offered by Belzona, are effective and cost-efficient methods for reducing the negative impacts of shipping.

bel5.jpeg

Belzona 7111 (Marine Grade) used to realign the main engine on a fishing boat with 500 tons of storage

Conclusion

A plethora of strategies will be necessary to achieve sustainable shipping. The quest for a sustainable fuel alternative, reducing underwater noise pollution, increasing efficiency, and the revolutionary use of coatings and composites are all integral strategies. Advanced polymeric solutions such as those produced by Belzona not only address critical issues such as cavitation and engine chocking but also offer a unique opportunity to revolutionise the industry. By simultaneously reducing capital expenditure, maintenance time and greenhouse gas emissions, these innovations play a pivotal role in steering the maritime sector towards a more sustainable and efficient future.

Using coatings and composites can revolutionise the maritime industry by simultaneously reducing capital expenditure and greenhouse gas emissions. Prioritising for the sake of the Blue Economy will propel the maritime industry into an era of environmental responsibility and economic resilience. Embracing these transformative solutions becomes not only a strategic imperative for the maritime industry but also a key enabler in realizing the holistic vision of a thriving Blue Economy that balances prosperity with responsible resource management.

Want to learn more about Belzona in the marine industry?

Click Here

The Importance of Calibrating Fixed Gas Detectors for Safety


Fixed gas detectors play a critical role in safeguarding people, places, and the planet against potentially life-threatening gases in environments ranging from high value industrial complexes to laboratories and hazardous confined spaces. However, to ensure their accuracy and reliability, regular calibration is an indispensable practice.

Calibration is usually a two-step procedure – the zero and the span. In the first step, the sensor is zeroed using ambient air after confirming that the target gas is not present or by using a suitable gas from a cylinder. The second step is to expose the instrument to the calibration gas that contains a known concentration of the target gas the sensor is designed to measure. The readings are then adjusted to match these values.

Whether an instrument warns and/or alarms at the proper time depends on its ability to translate the detected concentration of a target gas into an accurate reading

During calibration, gas detectors perform relative measurements. Rather than independently assessing the quantity of gas present, they measure the concentration of targeted gas within a test gas mixture by comparing real-time sensor response to the sensor’s response to a known concentration of target gas that the instrument is configured to detect and measure. This “known concentration” test gas serves as the instrument’s measurement scale, or reference point.

So, why is this important? Here are a few reasons to consider:

1. Ensuring Gas Measurement Accuracy and Reliability

A gas detector that isn’t accurately calibrated can lead to mis-readings, false alarms, and inadequate responses to hazardous situations. Proper calibration fine-tunes the detector’s sensor(s) to maximise speed of response, measurement accuracy, and provide reliable information to personnel required to make informed decisions in critical moments.

2. Meeting Regulatory Compliance

Safety regulations and standards are in place for a reason – to protect people, property, and the environment from potential hazards. Many industries are subject to these regulations that dictate the calibration and maintenance of gas detectors.

3. Mitigating False Alarms and Detection Failures

A poorly calibrated gas detector can lead to unnecessary evacuations, disruptions, and complacency due to frequent false alarms. Conversely, improper calibration might render a detector insensitive to dangerous gas levels, leaving people and operations vulnerable to potential harm.

4. Accounting for Changing Environmental Conditions

Fluctuations in temperature, humidity, and atmospheric pressure can impact the performance of these instruments. Regular calibration adjusts for these variables, ensuring that the sensor maintains its accuracy despite ever-changing conditions.

5. Combating Sensor Drift and Aging

Just like any mechanical or electronic component, gas sensors can experience signal drift or degradation over time. When the detector’s current readings deviate from the known reference, proper calibration procedures enable necessary adjustments to the sensor’s output. This adjustment effectively brings the sensor’s response back in line with the original calibration reference, minimising the impact of sensor drift.

6. Upholding Record Keeping and Liability

In the age of accountability, maintaining thorough records of gas detector calibration is a prudent practice. It demonstrates a commitment to safety management and can serve as a valuable resource in case of incidents or accidents. Having well-documented calibration records can potentially mitigate legal liabilities and bolster an organisation’s credibility.

7. Fostering Confidence in Safety Systems

An accurately calibrated gas detector is not just a piece of equipment; it’s a testament to an organisation’s dedication to safety. Regular calibration instils confidence in employees and management that the safety systems are in optimal condition, ready to provide accurate information and timely alerts in case of emergencies.

Conclusion

Routine calibration helps ensure accurate measurements, regulatory compliance, and a reliable defence against hazardous gases. Onsite safety and instrument availability is maximised while mitigating against false alarms at the same time. In a world where safety is paramount, the simple act of calibration speaks volumes about an organisation’s commitment to the well-being of its people and the environment.

Download our whitepaper: https://gb.msasafety.com/trucal#whitepaper


Rezitech Combats Tank Corrosion Under Insulation with Belzona Composite Wrap System

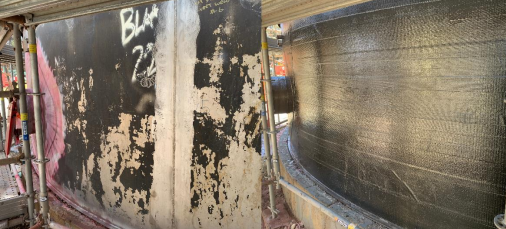
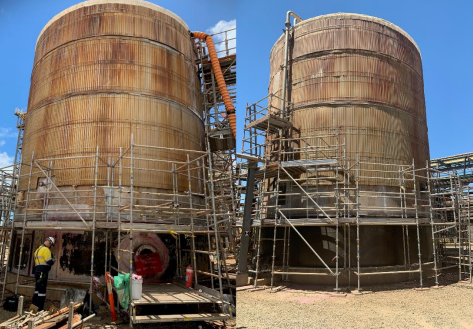
At a major global blue-chip nickel Mine in Australia, authorised Belzona Distributor, Rezitech, provided a full turnkey solution to combat corrosion under insulation on an ammonium sulphate feed tank. Within the space of 24 hours, the 9.5 metre (31.2 ft) diameter tank (with a height of 2 metres (6.6 ft) from ground level) was repaired and protected against future corrosion with the industrial composite wrap system, Belzona SuperWrap II.

fig1.jpeg

Figure 1. Composite wrap system curbs corrosion under insulation at nickel mine

Protective Coatings and Epoxy Repair Systems Support Transition to Net Zero

The Mine refines granulated nickel matte from their smelter into premium-grade nickel powder and briquettes containing 99.8% nickel. Nickel powder is further processed into nickel sulphate at a Refinery in Australia. Nickel sulphate is an essential ingredient in the lithium-ion batteries that drive electric vehicles (EVs). It could be argued that the increase in sales of EVs is one of the biggest climate wins of 2023. Indeed, according to the 2023 Report from Climate Action Tracker, of the 42 sectors which need

o achieve net zero status by 2050, the only sector which is on track is the share of EVs in lightduty vehicle sales. Considering how road transport currently accounts for 11% of global greenhouse gas emissions, EVs play a vital role in reducing these emissions.

As such, the polymeric technology required to repair and improve assets within the EV industry equally plays a vital role in supporting the transition to net zero. By repairing damaged assets instead of decommissioning and sending them to landfill, this significantly reduces the climate impact that would otherwise be incurred in this process.

Case Study: Feed Tank Suffering from Corrosion Under Insulation & SCC

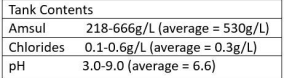
The Customer’s stainless steel feed tank was suffering from corrosion under insulation and chloride induced stress corrosion cracking. They required a solution that would not only restore the integrity on the substrate, but also protect the asset against future corrosion damage. Not only this, but as the tank operates at elevated temperatures of approximately 70°C (158°F) and processes highly corrosive medium, the repair solution would need to be able to withstand these harsh conditions.

fig2.jpeg

Figure 2. Tank Contents

Rezitech Specifies Belzona Composite Wrap Solution

Having worked with Rezitech over the course of five years, the Customer had complete confidence in the range of Belzona metal epoxy repair composites and industrial repair coatings the Distributorship offers. As such, they decided to contact them again for their advice and system recommendation

Following an inspection by Heath Westell, Sales Engineer at Rezitech, the composite wrap system, Belzona SuperWrap II, was specified.

Commenting on this specification, Heath said: “This composite wrap system is comprised of a fluid-grade resin system, a bespoke hybrid reinforcement sheet, based on fibre glass and carbon fibre, as well as a release film to compact and consolidate the application. The system is specially formulated to restore the strength of holed, weakened and corroded pipe and tank walls, making it the ideal solution for protecting the asset against corrosion under insulation for the long term. In addition, thanks to the cold-curing properties of the composite wrap system, this mitigates the need for hot work, making it a reliable alternative to welding.” 

Application Procedure:

Firstly, all traces of oil and grease contamination were removed using a suitable Rezitech Degreaser. Following this, the surfaces were grit-blasted to provide a surface cleanliness compliant with ISO 8501-1 SA 2½ (ASNZ 1627.4 class 2.5) with a minimum 75 µm (3 mil) rough angular profile.

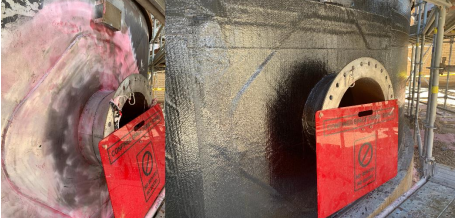
Once the surface was prepared, the Belzona 9381 reinforcement sheet was measured out and then wetted out with the Belzona resin system. The resin was then systematically applied to the areas to be repaired. Following this, the Belzona reinforcement sheets were then applied to the tank in three layers. The compression film was then added to the top of the application area. Next, using a roller, the Belzona SuperWrap II composite wrap system was then spread, rolled and compressed to the surface of the tank. The system was then left to cure for approximately eight hours.

fig3.jpeg

Figure 3. Stainless steel feed tank repaired and protected with Belzona SuperWrap II

Bypass the Need for Replacement with Polymeric Technology

By investing in the Belzona composite wrap solution, this enabled the Customer to successfully bypass the need to replace the corroded asset, and instead prolong the lifespan of the asset for years to come. Thus, this enabled the Customer to make significant savings in both time and money. In addition, given the important role EVs play in reducing global carbon emissions, it could be argued that polymeric technology also plays a fundamental role in supporting this transition by safeguarding the integrity of key assets within this industry.

fig4.jpeg

Figure 4. Mitigate the need for replacement with polymeric technology

About Rezitech: Established in 1968, Rezitech is the sole Australian Distributor for Belzona. Rezitech offers a comprehensive range of industrial protective coatings and epoxy metal repair composites to many different industries including: oil and gas, mining, power and facilities maintenance, amongst others. For more information, please visit: www.rezitech.com.au/products/belzona

Championing safety and efficiency in utility infrastructure

A focus on safety can expand work opportunities and open up a contractor to new and innovative business areas. KM Group, a prominent civil engineering contractor based across Wales and the South West of England, has carved a niche for itself in the industry through its specialisation in multi-utility mains installation, repair, and maintenance. Renowned for its commitment to safe working practices and ethical operations, KM Group partly puts its success down to its longstanding partnership with the supply chain risk management experts, Veriforce CHAS. 

In this case study, Murray Ambler-Shattock, Group Strategic Operations Manager at K M Group, explains how working with Veriforce CHAS has helped KM Group enhance its industry presence. He also discusses their shared objective to enhance safety and efficiency in the civil engineering sector, including through investment in the very latest technology.

CHAS accreditation and market access 

For several years, KM Group has been a proud partner of Veriforce CHAS, which has helped us to showcase our commitment to being a responsible and reliable contractor and enabled us to work with major contractors in our sector. Being accredited to CHAS Elite – which includes the Common Assessment Standard – shows we adhere to high standards across a wide range of risk areas, from health and safety to environmental management to equality, diversity, and inclusion. It also gives us a tool to set standards for our supply chain, so the contractors we work with are typically accredited to CHAS Standard or CHAS Advanced. Like Veriforce CHAS, at KM Group we are strong advocates of the Common Assessment Standard and its potential to improve efficiency and risk management standards in the construction sector. Veriforce CHAS was the first accreditation body to offer the assessment, and we were one of the first companies to complete it.

Accreditation isn't complicated - it's the golden ticket

Achieving accreditation is not a daunting task but a demonstration of our efficient business systems. In our experience, many organisations unknowingly already possess these systems in some form, and accreditation merely involves certifying their functionality.

Veriforce CHAS has been instrumental in conveying this message to our supply chain and supporting our contractors on their accreditation journey. This support is particularly beneficial for our smaller contractors, as CHAS Standard provides an entry-level accreditation that forms a solid foundation for future growth.

We view accreditation as the golden ticket, enabling business expansion and fostering collaboration with reputable employers. It establishes credibility and opens doors to valuable opportunities.

Raising industry standards 

Veriforce CHAS collaborates with clients like us to enhance overall compliance within supply chains. As contractors within our supply chains embark on their accreditation journey, they often aspire to achieve higher levels of accreditation, making them more appealing partners. This increased accreditation assures supply chain partners that these contractors are responsible businesses with effective risk management systems. This helps to raise standards overall and positively impacts the entire sector, creating a more conducive working environment for everyone involved.

Furthermore, there is a substantial effort through the Common Assessment Standard to enhance efficiency. This initiative aims to streamline the accreditation process, eliminating the need for contractors to undergo multiple assessments. Once contractors have completed the Common Assessment Standard through CHAS Elite, their certification becomes accessible through any of the accreditation providers, opening up even more opportunities for them. 


Innovation in utility infrastructure

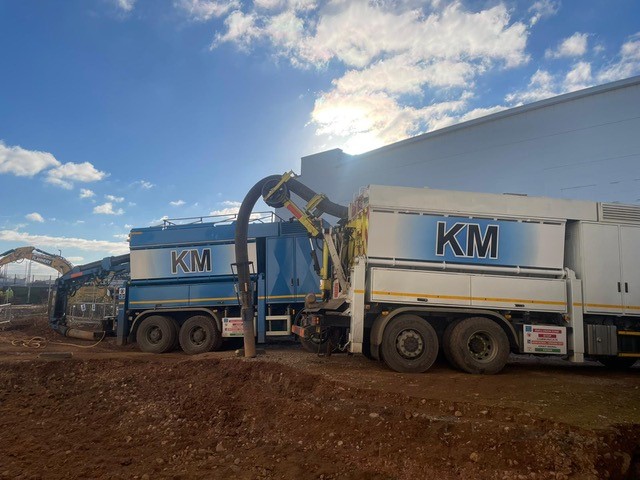
In recent years, KM Group has embarked on a journey of innovation by investing in Vacuum Excavation, a revolutionary technique transforming the Construction, Utility Infrastructure, and Civil Engineering sectors. This non-destructive digging method uses compressed air and a high-powered vacuum to excavate soil and materials gently. This is safer for operators and avoids the classic challenge of damaging pipes and cables, which can be extremely dangerous, as well as both costly and disruptive to a project. KM Group's adoption of vacuum extraction aligns with the industry trend of adhering to PAS 128 standards, significantly improving utility detection accuracy in the UK.


Pioneering vacuum excavation

KM Plant Hire & Groundworks Ltd, a subsidiary of KM Group, stands out as a leader in innovation within the Utilities Sector. Successfully implementing Vacuum Extraction in various locations, we have been championing safety, efficiency, and reliability in utility detection processes. This forward-thinking approach provides exceptional value to clients and positions KM Group as a pioneer in adopting innovative practices for safer and more efficient operations.

Conclusion

The journey of KM Group serves as a compelling case study in how strategic partnerships, such as our relationship with Veriforce CHAS, can propel a company to new heights. Through accreditation, KM Group has not only gained access to major industry projects but also uncovered hidden efficiencies within our operations. The adoption of Vacuum Excavation further solidifies our commitment to innovation and safety, and we believe it establishes us as a trailblazer in the ever-evolving landscape of utility infrastructure.

Find out more at: http://www.chas.co.uk/ or call 0345 521 9111.

https://km-group.co.uk or call 01633 415321